
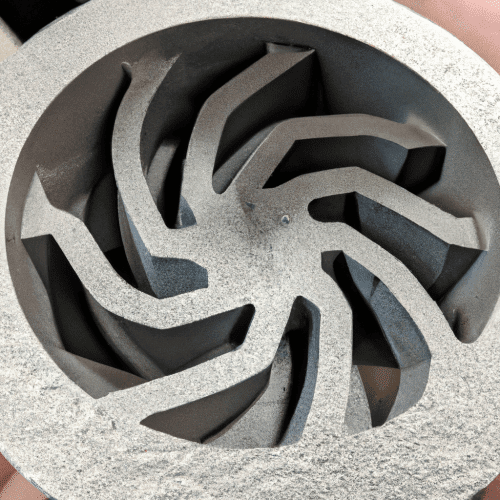
Additive manufacturing offers unparalleled design freedom and rapid prototyping capabilities, yet 3D printed parts often fall short in critical areas like dimensional accuracy, surface finish, and mechanical integrity. Integrating CNC machining into the post-processing workflow transforms these limitations, elevating part quality to meet stringent engineering specifications. This hybrid approach leverages the strengths of both technologies, producing components that are both complex and precise.
Achieving Precision and Tight Tolerances
While 3D printing excels at creating intricate geometries, its inherent layer-by-layer process introduces limitations in achieving consistently tight dimensional tolerances. Fused Deposition Modeling (FDM) parts, for instance, typically hold tolerances of ±0.5% or ±0.5 mm, whichever is greater, for features over 100 mm. Stereolithography (SLA) and Digital Light Processing (DLP) offer better precision, often achieving ±0.1 mm or ±0.2% for features under 100 mm, but still may not meet the demands of high-precision applications.
CNC machining provides the necessary corrective action, allowing for the removal of material to achieve significantly tighter tolerances. For plastic components, CNC milling can routinely hold tolerances of ±0.05 mm (±0.002 inches) or even ±0.025 mm (±0.001 inches) for critical features, depending on the material and machine rigidity. Metal parts machined on high-precision CNC equipment can achieve tolerances as tight as ±0.013 mm (±0.0005 inches) or better, far surpassing typical additive capabilities. This precision is crucial for mating parts, bearing fits, and assemblies requiring minimal clearance.
Strategic design for hybrid manufacturing involves adding extra material, or ‘stock,’ to critical surfaces during the 3D printing phase. This allows the CNC machine to precisely remove the excess, ensuring that features like holes, slots, and datum surfaces meet exact specifications. This method is particularly effective for parts with complex internal structures that are difficult to machine from solid stock but require external precision.
Superior Surface Finishes and Aesthetics
| Process | Typical Ra (µm) | Achievable Ra (µm) with CNC |
|---|---|---|
| FDM (Plastics) | 6.3 – 25 | 0.8 – 3.2 |
| SLA/DLP (Resins) | 1.6 – 6.3 | 0.4 – 1.6 |
| SLM/EBM (Metals) | 5 – 20 | 0.4 – 1.6 |
| CNC Machining (General) | 0.4 – 3.2 | N/A (Baseline) |
The layered nature of most 3D printing processes inherently results in anisotropic surface finishes, characterized by visible layer lines and a relatively high surface roughness (Ra value). FDM parts often exhibit Ra values ranging from 6.3 to 25 µm, while even high-resolution SLA prints might be in the 1.6 to 6.3 µm range. These finishes are often unacceptable for aesthetic components, fluid dynamic applications, or parts requiring low friction.
CNC machining effectively eliminates these surface imperfections, transforming the part’s exterior. Milling, turning, or grinding operations can achieve mirror-like finishes, with Ra values easily reaching 0.8 µm (32 microinches) or even 0.4 µm (16 microinches) for plastics and metals. This dramatically improves both the visual appeal and functional performance of the component, reducing drag, improving wear resistance, and enhancing sealing capabilities.
For optimal results, selecting appropriate cutting tools and machining parameters is essential. High-speed machining with sharp, multi-flute end mills for plastics, or specialized inserts for metals, can minimize chatter and achieve superior finishes. Coolant application is also critical, especially for plastics, to prevent material melting and ensure chip evacuation, contributing to a smoother final surface.
Integrating Precision Threads and Features
Creating accurate and robust threads directly through 3D printing can be challenging. Printed threads often lack the strength, precision, and smooth engagement required for reliable fastening, especially in load-bearing applications. The layer lines can interfere with thread engagement, leading to stripping or poor fit.
CNC machining provides a definitive solution for adding precision threads, bores, and other critical features post-print. Tapping or thread milling operations can create internal threads with high accuracy and strength, ensuring proper engagement with standard fasteners. External threads can be turned or milled with precise pitch and form, far exceeding the quality of printed threads.
Beyond threads, CNC can precisely machine critical bores for bearings, dowel pins, or shafts, ensuring concentricity and tight fit. Features like chamfers, fillets, and specific surface textures can also be added or refined, which might be difficult or impossible to achieve with additive processes alone. This capability is vital for components requiring precise mechanical interfaces.
Post-Processing Printed Metal Components
Metal additive manufacturing, such as Selective Laser Melting (SLM) or Electron Beam Melting (EBM), produces parts with excellent material properties but often with rough surfaces and near-net-shape geometries. These parts typically have Ra values between 5 and 20 µm, and require significant post-processing to meet functional requirements. CNC machining is indispensable for refining these metal prints.
The process involves stress relieving the printed metal part first, followed by fixturing and machining. Common operations include milling critical mating surfaces, drilling and reaming precision holes, and turning cylindrical features to achieve specified tolerances and surface finishes. This is particularly important for aerospace, medical, and automotive components where performance and reliability are paramount.
Machining parameters for printed metals often differ from those for wrought materials due to variations in microstructure and residual stresses. For example, 316L stainless steel printed via SLM might require adjusted feeds and speeds compared to its wrought counterpart to prevent tool wear and achieve desired surface integrity. Specialized cutting tools designed for difficult-to-machine alloys are frequently employed to manage the material’s characteristics effectively.
Modifying Critical Functional Surfaces
Many 3D printed components serve in applications where specific surfaces interact with other parts, bear loads, or require precise sealing. These ‘critical functional surfaces’ demand a level of accuracy and finish often beyond the capabilities of additive manufacturing alone. Examples include bearing seats, sealing faces, mounting interfaces, and cam surfaces.
CNC machining ensures these surfaces meet the exact geometric and surface finish requirements. For a bearing seat, for instance, CNC can achieve the precise diameter, roundness, and surface texture necessary for proper bearing fit and long-term performance. Without this post-processing, a printed bearing seat might lead to premature wear or failure due to poor fit or excessive friction.
The ability to precisely control material removal allows engineers to optimize contact areas, reduce stress concentrations, and ensure proper alignment in complex assemblies. This targeted modification enhances the overall reliability and lifespan of the hybrid manufactured part, making it suitable for demanding industrial applications where additive-only parts would fall short.