
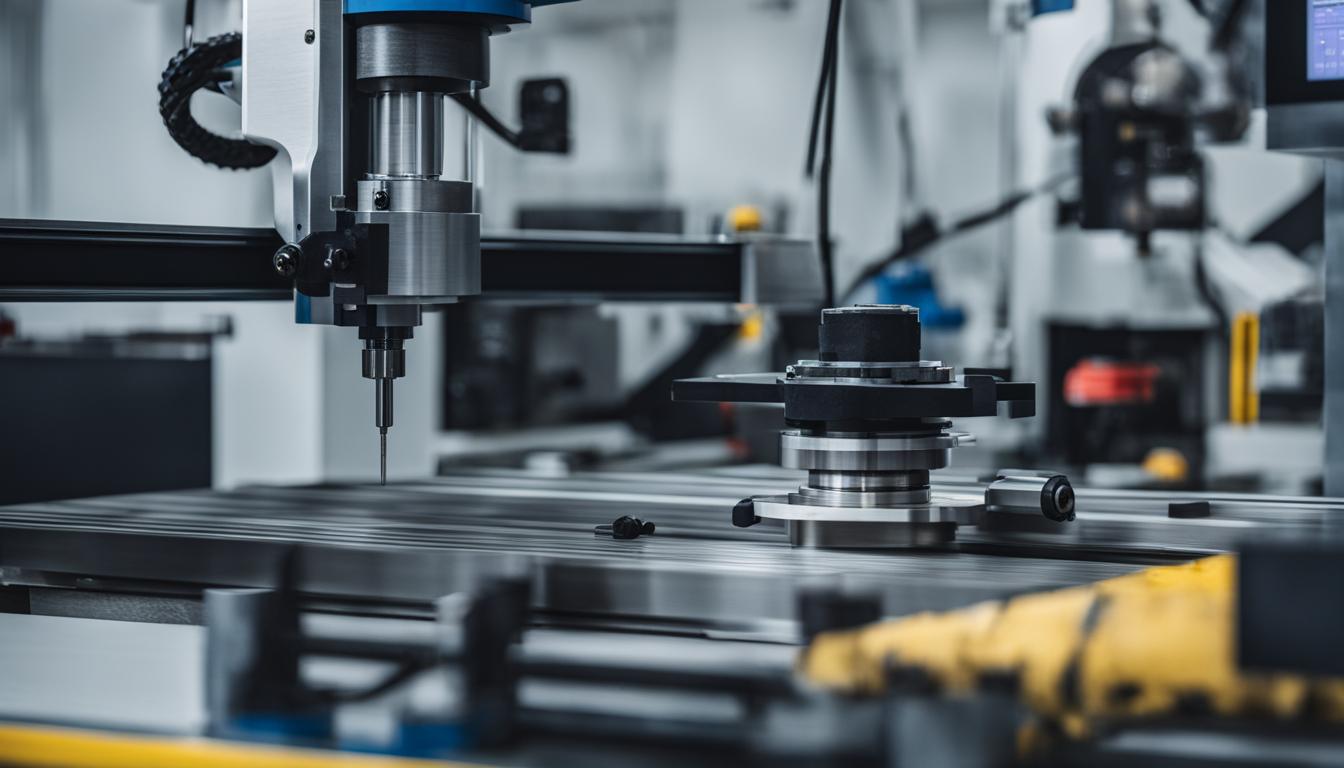
Maintaining stringent quality control is paramount in modern CNC machining to ensure parts meet exact specifications and perform reliably. Precision manufacturing demands a multi-faceted approach, integrating advanced inspection technologies and methodologies throughout the production lifecycle. This proactive strategy minimizes defects, reduces scrap, and optimizes overall operational efficiency.
Implementing robust quality control measures during and after the CNC machining process is not merely about detecting errors; it is about preventing them. By leveraging sophisticated tools and data-driven techniques, manufacturers can achieve consistent, high-quality output, critical for industries like aerospace and medical devices.
In-Process Spindle Probing
In-process spindle probing integrates measurement directly into the CNC machine, allowing for automated inspection without removing the workpiece. This technology uses a precision touch or scanning probe mounted in the spindle, much like a cutting tool, to gather dimensional data. It significantly reduces non-productive time by automating part and tool setting, eliminating manual errors.
Spindle probes are instrumental in verifying workpiece position, setting work offsets, and measuring critical features during machining operations. They can detect issues such as incorrect billet loading, stock orientation, or even tool wear before a significant number of defective parts are produced. This immediate feedback loop enables real-time compensation and process adjustments.
Common types of CNC probes include touch-trigger probes, which provide a single XYZ coordinate upon contact, and analog scanning probes that capture continuous surface data. These probes transmit signals via optical, radio, or hard-wired systems to the machine controller. High-accuracy industrial probes, such as those from Renishaw, can achieve repeatability down to 0.25 micrometers for high-precision applications.
The benefits of spindle probing extend to reduced setup times, improved part consistency, and decreased scrap rates. By verifying the setup before cutting and monitoring the process in-situ, manufacturers gain greater confidence that the physical machining process aligns with the programmed one, preventing costly collisions and rework.
Coordinate Measuring Machines (CMM)
| Machining Process | Typical Ra (µm) | Typical Ra (µinch) |
|---|---|---|
| Milling | 0.8 – 6.3 | 32 – 250 |
| Turning | 0.8 – 6.3 | 32 – 250 |
| Grinding | 0.2 – 1.6 | 8 – 63 |
| Lapping/Polishing | 0.025 – 0.4 | 1 – 16 |
| Reaming | 0.8 – 3.2 | 32 – 125 |
Coordinate Measuring Machines (CMMs) are indispensable for precise post-process inspection of complex geometries, offering highly accurate three-dimensional measurements. These machines operate by sensing discrete points on an object’s surface with a probe, then recording their X, Y, and Z coordinates to determine dimensional accuracy.
Various CMM types exist, each suited for specific applications. Bridge-type CMMs are the most common, known for their structural rigidity and high accuracy, ideal for medium to large parts. Gantry CMMs are scaled-up versions for very large components, while cantilever and horizontal arm CMMs offer better access for smaller or long, slender parts, respectively.
Modern CMMs utilize diverse probing systems, including contact touch-trigger probes, scanning probes, and non-contact optical or laser sensors. These systems enable comprehensive evaluation of Geometric Dimensioning and Tolerancing (GD&T) features like flatness, perpendicularity, and true position against CAD models.
Achieving optimal CMM accuracy, typically ranging from ±1 to ±5 µm for standard systems and sub-micron for ultra-precision models, relies on rigorous environmental controls. Maintaining controlled lab conditions at 20°C (68°F) is the ISO standard for CMM operation, minimizing thermal expansion and vibration effects. Annual calibration by certified technicians is also crucial for maintaining accuracy.
Surface Roughness Testing
Surface roughness significantly impacts a part’s functional performance, affecting friction, wear, sealing behavior, and coating adhesion. Quantifying these fine irregularities is essential for critical components, ensuring they meet design specifications for their intended application.
Common parameters used to describe surface roughness include Ra (arithmetic mean roughness), Rz (maximum peak-to-valley height), and Rq (root mean square roughness). Ra is the most widely specified for general comparison, while Rz is critical for sealing and fatigue-sensitive surfaces due to its sensitivity to isolated defects. Rq, which weights larger deviations more heavily, is often used in optics and semiconductor applications.
Surface roughness is typically measured using stylus profilometers, where a diamond-tipped stylus physically traces the surface profile. Optical or non-contact profilometers, utilizing white light interferometry or confocal microscopy, are employed for delicate or soft surfaces, mapping the surface without physical contact.
Industry standards like ASME B46.1 and ISO 4287 provide guidelines for surface texture measurement and interpretation. For critical components, specifying multiple parameters offers a more complete and reliable picture of surface quality than any single value alone.
Statistical Process Control (SPC)
Statistical Process Control (SPC) is a methodology that uses statistical methods to monitor and control a process, ensuring it operates efficiently and produces conforming products. It moves quality departments from a reactive inspection mindset to proactive defect prevention.
Key SPC tools include control charts, such as X-bar and R charts, which help distinguish between common cause variation (natural to the process) and special cause variation (indicating a problem). By continuously collecting and analyzing production data, SPC detects and corrects deviations early, preventing defective parts from being produced.
Implementing SPC in CNC machining involves establishing baselines during First Article Inspection, ongoing sampling, and real-time analysis of control charts. This data-driven approach allows operators to identify trends before parts exceed tolerance limits, enabling timely process adjustments.
The benefits of SPC are substantial, including reduced variability, increased productivity, and lower costs due to minimized rework and scrap. In precision machining operations, SPC has been shown to significantly reduce out-of-spec parts and improve overall process stability.
First Article Inspection (FAI)
First Article Inspection (FAI) is a critical production validation process that verifies a new or modified manufacturing process can consistently produce parts meeting all engineering and specification requirements. It is a comprehensive review of the engineering documentation and the manufacturing process from raw materials through functional testing.
FAI is typically required for new product introductions, significant design or process changes, or when production is transferred to a different facility or supplier. This inspection ensures the production process is properly set up before full-scale manufacturing begins, identifying any issues early to avoid costly corrections later.
The FAI process involves a detailed examination of the first sample produced, often documented in a First Article Inspection Report (FAIR). This report includes verified measurements of characteristics, material and process specifications, and other checklist items as required by the customer.
In aerospace and defense industries, FAI is defined by the AS9102 standard, which provides a structured framework for documenting conformance to design specifications. This standard ensures objective evidence that the manufacturing process can deliver repeatable, conforming products, reducing future product escapes and minimizing supply chain risks.