
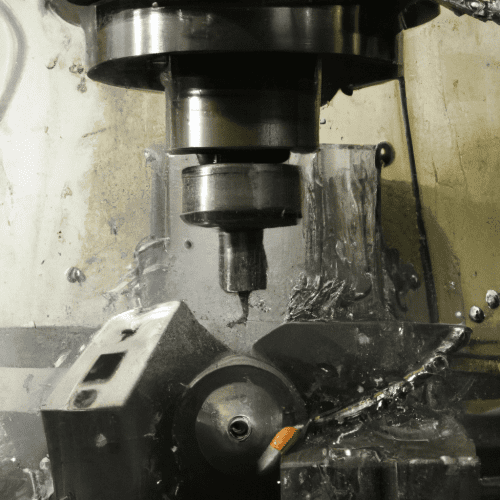
Machining represents a fundamental manufacturing process where material is systematically removed from a workpiece to achieve a desired final shape, size, and surface quality. This subtractive method is critical across numerous industries, including aerospace, automotive, and medical devices, forming the backbone of precision engineering.
The core principle involves controlled mechanical interaction between a cutting tool and the material surface. This interaction generates chips as waste products, distinguishing machining from additive manufacturing processes like 3D printing, which build parts layer by layer.
The Core of Subtractive Manufacturing
Subtractive manufacturing is a time-tested method for creating parts by removing material from a solid block, often called a blank or workpiece. Engineers utilize this approach to achieve tight tolerances, superior surface finishes, and robust material performance.
This process encompasses various techniques, including CNC milling, CNC turning, drilling, and grinding. Each method employs specialized tools and machine settings to precisely shape metals, plastics, and composites, ensuring the final component meets stringent design specifications.
The typical workflow for subtractive manufacturing involves material selection, toolpath programming, roughing and finishing operations, and rigorous inspection. Computer-Aided Design (CAD) models are converted into machine-readable instructions, such as G-code, guiding the machine’s movements with high accuracy.
Understanding Material Removal Mechanics
| Characteristic | Turning | Milling |
|---|---|---|
| Workpiece Movement | Rotates | Stationary (typically) |
| Tool Movement | Stationary, moves linearly | Rotates, moves along multiple axes |
| Primary Geometry | Cylindrical, rotational | Complex, planar, prismatic |
| Typical Tolerance (inches) | ±0.002” | ±0.005” |
| Standard Surface Finish (Ra μm) | 0.8 – 1.6 μm | 1.6 – 3.2 μm |
Material removal in machining primarily occurs through shear deformation. A sharp cutting edge penetrates the workpiece, generating stresses that exceed the material’s shear strength, causing material to separate as chips.
Key mechanical elements governing this process include the relative motion between the tool and workpiece, the cutting forces exerted, chip formation and evacuation, and heat generation due to plastic deformation and friction. Tool geometry, including rake and clearance angles, significantly influences cutting efficiency and surface integrity.
Controlling these parameters is essential to prevent issues like excessive forces, heat accumulation, or vibration, which can lead to dimensional inaccuracies, surface degradation, or premature tool failure. Modern CNC systems continuously monitor and adjust these factors for optimal performance.
Precision Shaping Through Mechanical Engagement
Precision part shaping relies heavily on the controlled mechanical engagement of cutting tools. The interaction between the tool’s cutting edges and the workpiece material dictates the accuracy and quality of the finished component.
Tool engagement refers to how much of the cutting tool is in contact with the material at any given moment. Factors like radial depth of cut, cutter diameter, and cutting edge angle influence the mechanical load on the tool and the resulting chip thickness.
Optimizing tool engagement is crucial for maximizing tool life, productivity, and process reliability. Advanced CAM software and CNC equipment utilize techniques like trochoidal milling and constant tool engagement tool paths to manage intermittent loads, especially in complex geometries.
Turning Operations: Rotational Material Removal
Turning is a machining process primarily used to produce cylindrical or rotationally symmetric components. In this operation, the workpiece rotates while a stationary, single-point cutting tool moves along its surface, removing material.
Lathes are the machines specifically designed for turning, capable of reducing part diameter or length. Common parts created through turning include shafts, bushings, and threads, often held in a chuck or between centers for high concentricity.
Feeds and speeds in turning are critical parameters. Surface speed (SFM) is converted to spindle RPM based on the workpiece diameter, while feed rate is typically measured in inches per revolution (IPR) or millimeters per revolution (mm/rev). For steels, typical parting feed rates can be around 0.001 in/rev, while for plastics, they might be up to 0.005 in/rev.
Milling Operations: Multi-Axis Material Shaping
Milling is a subtractive manufacturing process that employs a rotating multi-point cutting tool to remove material from a stationary workpiece. This method is highly versatile, ideal for creating complex shapes, planar features, pockets, slots, and intricate contours.
CNC milling machines offer various axes of movement (e.g., 3-axis, 5-axis) allowing for the fabrication of highly detailed and multi-faceted parts. The process begins with securing the workpiece, installing appropriate milling tools like end mills or face mills, and executing computer-programmed toolpaths.
Feeds and speeds for milling are calculated based on surface feet per minute (SFM), tool diameter, chip load per tooth, and the number of flutes. For instance, a 1/2″ 4-flute carbide end mill in 6061 aluminum might run at 6,112 RPM with a feed rate of 97.8 IPM, assuming an 800 SFM and 0.004″ chip load per tooth. These parameters are adjusted for material, tool rigidity, and desired surface finish.
Standard machining tolerances are defined by organizations like ISO 2768 and ASME Y14.5, ensuring consistency across manufacturers. A general tolerance of ±0.005” (±0.127 mm) is widely accepted for standard milling, while turning can achieve tighter tolerances, often around ±0.002” (±0.051 mm).
Surface finish is a critical consideration, specified by parameters like Ra (Average Roughness). A standard machined finish is typically 3.2 μm Ra, suitable for many applications. Tighter finishes, such as 0.8 μm Ra or smoother, require more advanced techniques and often increase production costs.