
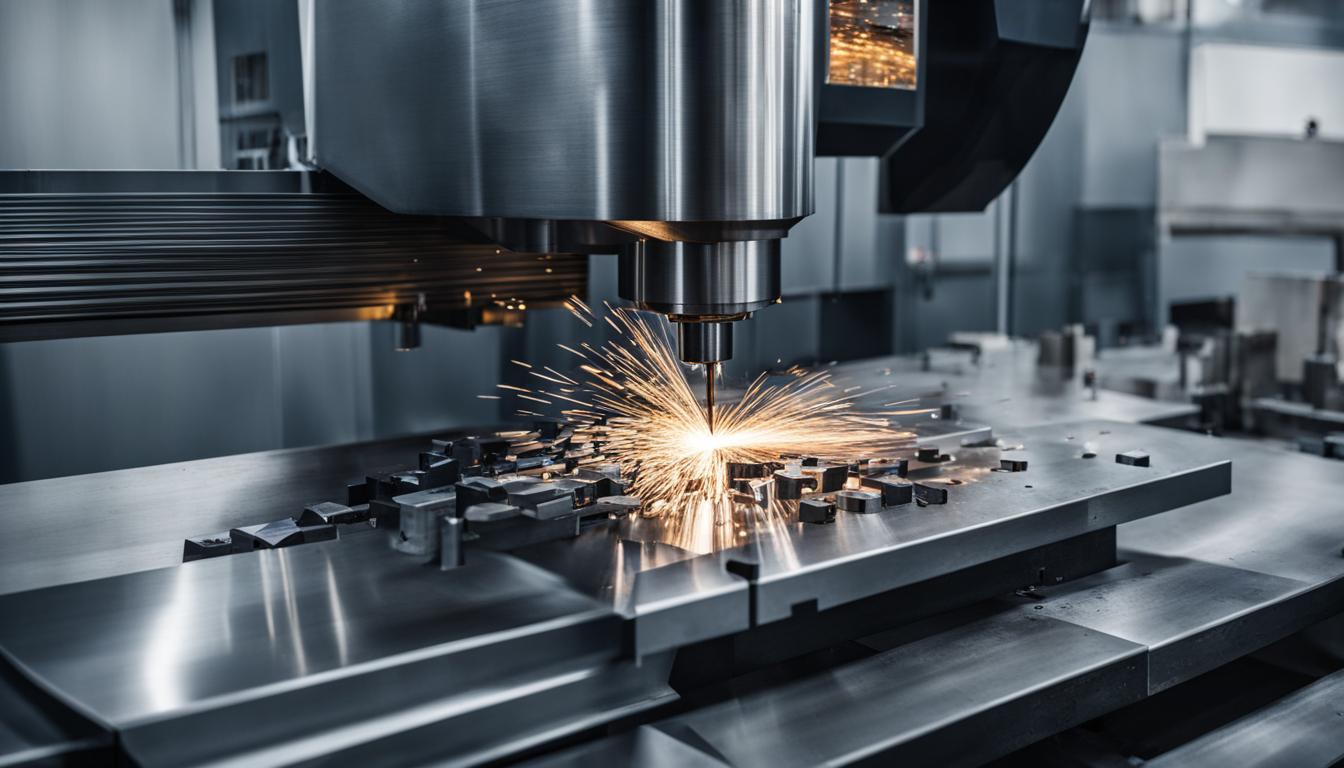
A Vertical Machining Center (VMC) represents a cornerstone of modern subtractive manufacturing, primarily distinguished by its vertically oriented spindle. This configuration allows cutting tools to approach the workpiece from above, making it highly effective for machining flat surfaces, pockets, and intricate features on one side of a part.
These robust machines integrate advanced computer numerical control (CNC) systems to execute precise, repeatable machining operations. Their design prioritizes rigidity and accuracy, essential for producing components with tight tolerances across various industries.
Vertical Spindle Orientation Fundamentals
The defining characteristic of a VMC is its spindle’s vertical alignment, which positions the cutting tool perpendicular to the worktable. This setup provides excellent chip evacuation, as gravity assists in removing chips from the cutting zone, preventing re-cutting and improving surface finish.
This orientation also offers superior visibility of the machining process, aiding in setup and inspection. Tool access is generally straightforward, simplifying programming for many common milling operations like face milling, slotting, and drilling.
Modern VMCs feature high-speed spindles, often reaching 15,000 to 20,000 RPM or more, enabling efficient material removal and finer surface finishes, particularly with smaller diameter tools. Spindle taper sizes, such as CAT40, BT40, or HSK63, dictate tool holding capacity and rigidity.
Understanding 3-Axis VMC Table Movement
| Parameter | Aluminum (6061-T6) | Mild Steel (1018) | Stainless Steel (304) |
|---|---|---|---|
| Spindle Speed (RPM) | 8,000 – 15,000 | 2,000 – 5,000 | 1,500 – 4,000 |
| Feed Rate (IPM) | 50 – 200 | 10 – 40 | 5 – 25 |
| Axial Depth of Cut (ADOC) | 0.5 – 1.5 x Diameter | 0.2 – 0.8 x Diameter | 0.1 – 0.5 x Diameter |
| Radial Depth of Cut (RDOC) | 0.1 – 0.3 x Diameter | 0.05 – 0.2 x Diameter | 0.03 – 0.15 x Diameter |
Standard 3-axis VMCs operate with movement along the X, Y, and Z axes. The X-axis typically controls left-to-right movement of the worktable, while the Y-axis manages front-to-back motion. The Z-axis, crucial for depth control, moves the spindle head vertically up and down.
This coordinated movement allows the cutting tool to traverse the workpiece in three dimensions, creating complex geometries by interpolating these linear motions. The workpiece remains stationary on the table during machining, with all motion provided by the table and spindle head.
Typical work envelope dimensions for a medium-sized VMC might include X-axis travel of 20-40 inches, Y-axis travel of 15-25 inches, and Z-axis travel of 15-20 inches. Rapid traverse rates, indicating the speed at which axes move when not cutting, can exceed 1,000 inches per minute (IPM) on high-performance machines.
Automatic Tool Changers Enhance Productivity
Automatic Tool Changers (ATCs) are integral to VMC automation, allowing the machine to swap cutting tools without manual intervention. This capability significantly reduces cycle times and enables continuous, unattended operation for complex multi-tool jobs.
ATCs typically consist of a tool magazine, which stores a variety of tools, and a mechanism to transfer tools between the magazine and the spindle. Magazine capacities range from 20 to over 60 tools, accommodating diverse machining requirements.
Tool change times are a critical performance metric, with modern VMCs achieving tool-to-tool changes in under 2 seconds and chip-to-chip times (including spindle acceleration/deceleration) often below 5 seconds. This efficiency is vital for maximizing throughput in high-volume production environments.
Enclosed Chip Guards Ensure Safety and Cleanliness
Every VMC features a fully enclosed chip guard enclosure, a fundamental safety and operational component. This robust barrier contains metal chips, coolant, and airborne particles generated during the machining process, protecting operators and the surrounding environment.
Beyond safety, the enclosure maintains a cleaner workshop by preventing the spread of machining debris. It also facilitates efficient coolant management, directing coolant back into the machine’s filtration system for recirculation, which extends tool life and improves surface finish.
These enclosures are designed with interlocked doors that prevent machine operation when open, adhering to strict safety standards like ISO 23125 and OSHA regulations. Integrated lighting and viewing windows allow operators to monitor the process safely without exposure to hazards.
Strategies for Milling Complex Parts on a VMC
While 3-axis VMCs excel at machining parts with features accessible from a single setup, they can also produce surprisingly complex geometries through strategic workholding and multiple setups. This often involves rotating the workpiece to present different faces to the spindle.
Effective CAM programming is essential for optimizing tool paths and minimizing setup changes. Utilizing advanced cutting tools, such as high-helix end mills or specialized form tools, can also enhance efficiency and part quality for intricate features.
Achieving tight tolerances on complex parts requires careful consideration of machine rigidity, thermal stability, and tool deflection. Standard VMC positioning accuracy typically ranges from ±0.0002 to ±0.0004 inches, with repeatability often within ±0.0001 inches.