
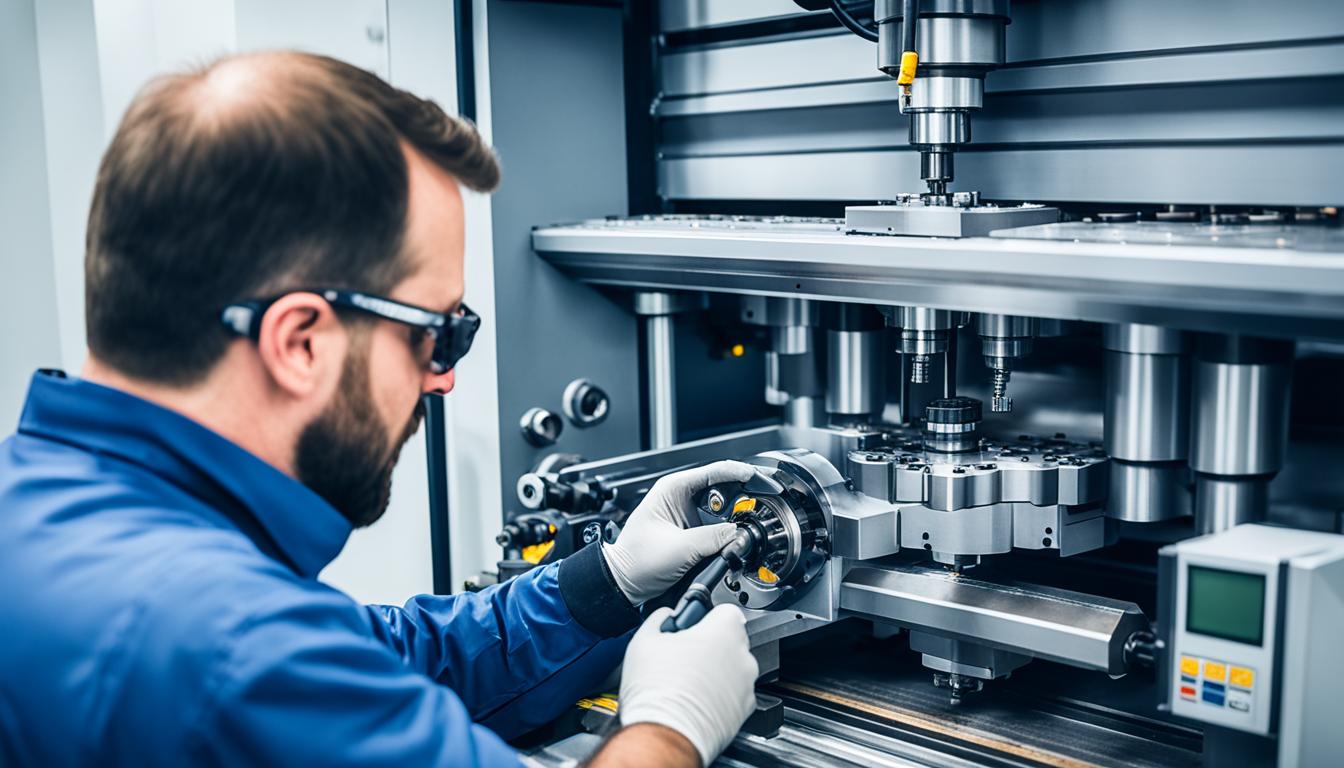
Consistent, proactive maintenance is paramount for ensuring the longevity and precision of Computer Numerical Control (CNC) machinery. Neglecting routine checks and preventative measures can lead to costly downtime, diminished part quality, and premature component failure. Implementing a structured maintenance regimen safeguards your investment and maintains operational efficiency.
Each critical system within a CNC machine requires specific attention, from the high-speed spindle to the coolant delivery. Adhering to manufacturer guidelines and industry best practices for lubrication, filtration, and component inspection directly translates to extended machine life and consistent output quality.
Spindle Lubrication Protocols
Spindle lubrication is fundamental to minimizing friction and wear within the high-speed rotating assembly. Modern CNC spindles typically employ either grease lubrication or oil-air/oil-mist systems, each with distinct characteristics and maintenance requirements. Grease-lubricated spindles, often found in medium-speed applications, are packed with high-viscosity lubricants designed for extended intervals, offering simplicity and lower initial cost.
High-speed spindles, particularly those exceeding 10,000 RPM, frequently utilize oil-air or oil-mist lubrication systems. Oil-air systems deliver precise, controlled amounts of oil suspended in compressed air directly to the bearings, providing superior cooling and continuous lubrication for stable performance and extended bearing life. Oil-mist systems, while effective, are gradually being phased out due to environmental concerns.
Daily checks for oil-lubricated spindles involve visually inspecting the reservoir level and verifying that the automatic lubrication system is dispensing oil correctly. A typical oil-air system might deliver oil at a rate of 20 drops per minute, though this can vary from 5 to 80 drops depending on the application. Any deviation from the recommended level or an alarm indicating low pressure or an empty reservoir warrants immediate investigation.
Inadequate spindle lubrication leads to increased friction, excessive heat generation, and accelerated bearing wear, potentially causing catastrophic spindle failure. Regular monitoring and adherence to the manufacturer’s specified lubricant type and viscosity (e.g., ISO VG32 or ISO VG68 for many CNC machines) are crucial for optimal performance and longevity.
Way Lube System Management
| Tolerance Level | Imperial (inches) | Metric (mm) |
|---|---|---|
| Standard Machining | ±0.005″ to ±0.010″ | ±0.127 mm to ±0.254 mm |
| Precision Machining | ±0.001″ to ±0.002″ | ±0.0254 mm to ±0.0508 mm |
| Tight Tolerance Machining | ±0.0001″ to ±0.0005″ | ±0.0025 mm to ±0.0127 mm |
The way lubrication system protects the linear guides, ball screws, and other moving components from friction and wear, ensuring smooth, accurate axis movement. This automatic oiler system is critical, yet often overlooked until an alarm signals an empty tank. However, an alarm might not trigger if the system is clogged or a line is broken, leading to prolonged operation without lubrication.
Refilling the way lube oil reservoir should be a routine task, typically performed daily or weekly depending on machine usage. It is essential to use the manufacturer-recommended way oil, often specified by ISO Viscosity Grade (VG), such as ISO VG 32, 68, or 220. These oils are formulated to provide the necessary film strength and adhesion for machine tool slideways.
Beyond simply refilling, technicians must verify the automatic lubrication pump’s functionality. This includes checking for proper distribution flow, inspecting for clogged filters within the pump, and ensuring all oil lines are intact and delivering lubricant to the metering units. A pressure gauge on the pump can indicate proper system operation during the pumping cycle.
Failure of the way lube system can manifest as positioning or repeatability problems, axis noise, or even axis drive motor overload alarms. Consistent lubrication prevents premature wear of critical components, maintaining the machine’s geometric accuracy and extending its operational life.
Ball Screw Backlash Assessment
Backlash in a ball screw assembly refers to the axial play or ‘lost motion’ between the screw and the nut when the direction of rotation reverses. This clearance, even if minimal, directly impacts a CNC machine’s positioning accuracy, surface finish, and repeatability, especially in tight-tolerance applications.
Measuring backlash accurately requires specific tools and methods. A common approach involves using a magnetic base and a dial indicator with a resolution of at least 0.001mm (1 micron). The ‘push-pull’ test involves locking the screw, placing the indicator against the moving table, and manually applying force in both directions to read the total movement.
Another method, the ‘reversal’ test, dynamically measures lost motion during actual machine operation. This involves jogging the machine in one direction, zeroing the indicator, commanding a small precise movement, and then reversing the direction to observe the delay before the table moves. Modern CNC controls can also perform programmed motion tests to measure backlash.
Standard backlash values below 0.01 mm (0.0004 in) are generally acceptable for light machining, while values exceeding 0.02 mm (0.0008 in) often compromise contour accuracy and hole positioning. Excessive backlash can stem from worn ball screws and nuts, loose bearings or couplings, or insufficient lubrication. Addressing significant backlash may involve adjustment, compensation through CNC software, or ultimately, component replacement.
Electrical Cabinet Air Filtration
Maintaining a clean electrical cabinet is crucial for the reliable operation and longevity of sensitive electronic components within a CNC machine. Dust, debris, and coolant mist can accumulate on circuit boards and heat sinks, leading to overheating, short circuits, and premature component failure. Effective air filtration prevents these contaminants from entering the cabinet.
Electrical cabinet filters, typically made of pleated media, foam, or mesh, require regular cleaning or replacement. The frequency depends on the operating environment; dusty or humid conditions necessitate more frequent attention. A visual inspection should be part of a daily or weekly maintenance routine, with cleaning or replacement scheduled as needed.
Cleaning involves carefully removing the filters and using compressed air to blow out accumulated dust and debris. For washable filters, a mild detergent and water can be used, ensuring they are completely dry before reinstallation. Replacing filters with the correct type and size is essential to maintain the cabinet’s protective seal and airflow.
Neglecting electrical cabinet filtration can lead to significant issues. Overheated components experience reduced lifespan, and dust can act as an insulator, exacerbating thermal problems. Furthermore, conductive dust combined with humidity can cause electrical arcing, resulting in costly damage and unexpected machine downtime.
Coolant Tank Maintenance
The coolant system is vital for heat reduction, lubrication, and chip evacuation during machining. Proper coolant tank maintenance directly impacts tool life, part quality, and the overall health of the CNC machine. Neglected coolant can lead to a host of problems, including bacterial growth, foul odors, corrosion, and reduced machining performance.
Daily checks should include monitoring the coolant level in the sump and topping it off with properly mixed coolant. Visual inspection for tramp oil accumulation on the surface is also critical, as tramp oil provides a food source for bacteria and reduces the coolant’s effectiveness.
Weekly, or as recommended by the coolant supplier, concentration and pH levels must be tested using a refractometer and pH strips. Maintaining the manufacturer-recommended concentration (typically 5-10%) prevents issues like excessive foaming or reduced cooling/lubrication. pH levels should remain within the optimal range (usually above 8.0 for ferrous materials) to prevent corrosion and inhibit bacterial growth.
Regular removal of tramp oil using skimmers (belt, disc, or tube type) or coalescers is essential to extend coolant life and prevent bacterial proliferation. Furthermore, periodic deep cleaning of the coolant tank is necessary to remove accumulated chips, fines, sludge, and biofilm that harbor bacteria and re-contaminate fresh coolant.
A comprehensive tank cleaning involves draining all coolant, physically removing bulk contamination, circulating an alkaline cleaner through the entire system, rinsing thoroughly, and then recharging with a fresh, correctly mixed coolant batch. Implementing effective filtration systems, such as bag or cartridge filters, also helps remove chips and fine particles, further extending coolant life and preventing issues like tool wear and poor surface finishes.