Choosing a hobby milling machine requires careful consideration of several critical engineering parameters. The machine’s fundamental design directly impacts its precision, material removal rates, and overall longevity. Prospective owners must evaluate structural integrity, motor specifications, and software compatibility to ensure the mill meets their project demands.
Assessing Machine Rigidity and Construction
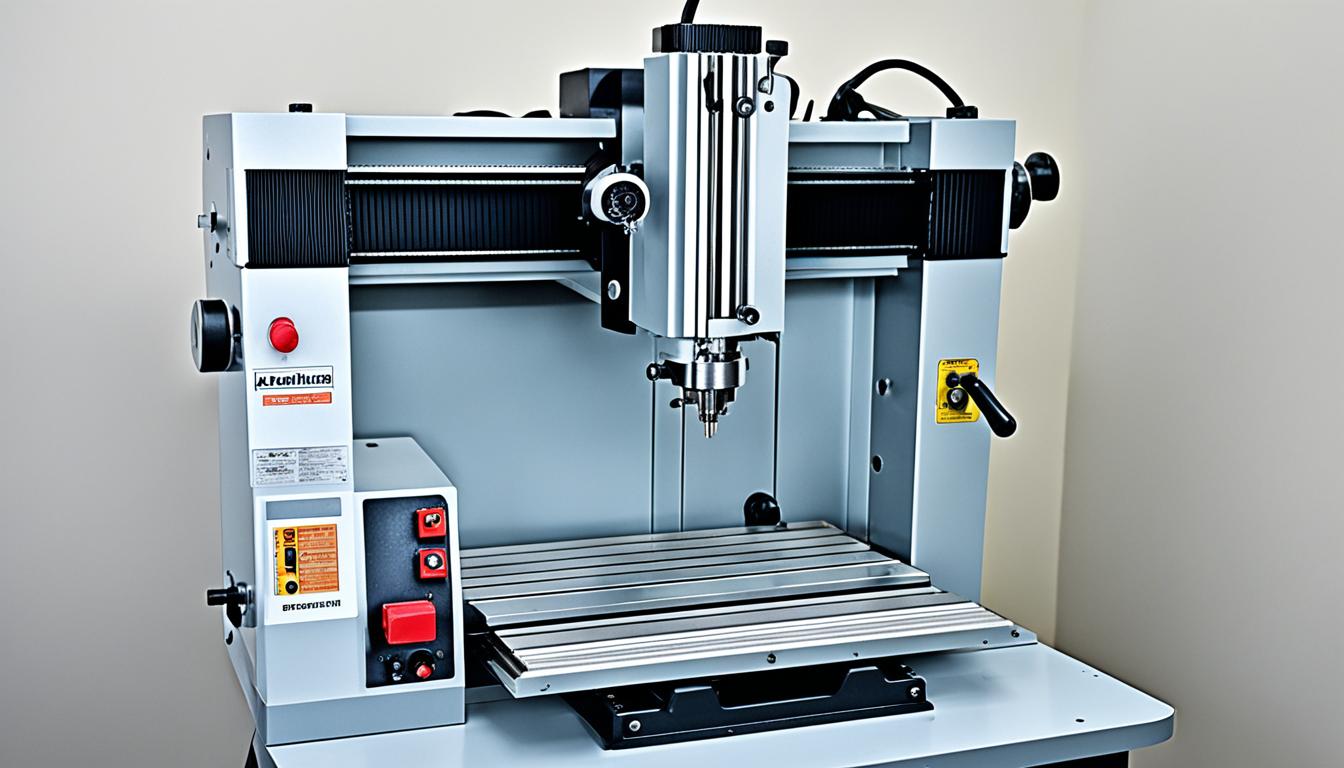
Frame rigidity is paramount for achieving accurate cuts and minimizing tool chatter in any milling operation. Hobby machines typically feature cast iron or heavy steel frames, with cast iron generally offering superior vibration dampening due to its inherent material properties. A robust, heavy base and column are essential for maintaining stability during aggressive machining.
The design of the machine’s ways significantly influences its precision and durability. Dovetail ways, common on many benchtop mills, provide excellent contact area and adjustability for wear, contributing to long-term accuracy. Box ways, while less common in the hobby segment, offer even greater rigidity and load-bearing capacity, though they are often found on larger, industrial-grade equipment.
Machine weight often correlates directly with rigidity; heavier machines generally absorb cutting forces more effectively. A typical hobby mill suitable for light metalwork might weigh between 150 and 300 pounds, providing a stable platform for various materials. The column’s thickness and its attachment method to the base are also critical, preventing deflection under load.
Understanding Spindle Power and Performance
| Parameter | Aluminum (6061) | Mild Steel (1018) | Engineering Plastics (Delrin) |
|---|---|---|---|
| Spindle Speed (RPM) | 3000 – 8000 | 800 – 2000 | 4000 – 10000 |
| Feed Rate (IPM) | 15 – 40 | 3 – 10 | 20 – 60 |
| Depth of Cut (per pass) | 0.020 – 0.040′ | 0.005 – 0.015′ | 0.050 – 0.100′ |
| Surface Finish | Good to Excellent | Fair to Good | Excellent |
The spindle motor’s power dictates the machine’s ability to cut different materials at appropriate speeds and depths. For hobby milling, DC brush motors are common, offering variable speed control, but brushless DC (BLDC) motors are gaining popularity for their higher efficiency, quieter operation, and improved torque characteristics across the RPM range.
When cutting aluminum, a hobby mill typically requires a spindle motor of at least 0.5 horsepower (approximately 370 watts) to achieve reasonable material removal rates without bogging down. Machining mild steel, however, demands more power, with 1.0 to 1.5 horsepower (750 to 1100 watts) being a more suitable minimum for effective cutting and tool life.
Spindle speed range is another vital specification. A broad RPM range, from around 100 RPM for large diameter drilling or tapping to 5,000-10,000 RPM for small end mills in aluminum, provides versatility. Direct drive spindles offer higher efficiency and less runout compared to belt-driven systems, though belt drives can provide more torque at lower speeds.
Here are typical spindle power requirements for common hobby milling tasks:
- Aluminum Machining: 0.5 – 1.0 HP (370 – 750 W)
- Mild Steel Machining: 1.0 – 1.5 HP (750 – 1100 W)
- Harder Steels/Titanium (light cuts): 1.5 HP+ (1100 W+)
Optimizing Worktable Capacity for Projects
The worktable’s size and travel capacity define the maximum dimensions of parts a machine can handle. Hobby mills vary significantly, but a common work envelope for a versatile benchtop unit might offer X-axis travel of 12-16 inches, Y-axis travel of 6-8 inches, and Z-axis travel of 8-10 inches. These dimensions accommodate a wide array of small to medium-sized projects.
Consider the physical dimensions of your most frequent projects. A larger worktable provides more flexibility for fixturing multiple parts or machining larger single components. However, increased table size often correlates with a larger machine footprint and higher cost, so balancing capacity with available workshop space is crucial.
The table’s T-slot configuration and spacing are also important for workholding. Standard T-slots (e.g., 1/2-inch or 12mm) allow for common clamps and vises. Ensure the table is ground flat and parallel to the spindle for optimal accuracy, as any deviation will directly impact part quality.
Leveraging Community Software Ecosystems
Software support is a critical, often overlooked, aspect of hobby CNC milling. The ecosystem includes CAD (Computer-Aided Design) for part creation, CAM (Computer-Aided Manufacturing) for generating toolpaths, and control software for executing G-code on the machine. Strong community support ensures access to tutorials, troubleshooting, and shared knowledge.
Fusion 360 remains a highly popular choice for hobbyists, offering integrated CAD/CAM capabilities with a robust free tier for personal use. Its extensive online community and tutorials make it accessible for beginners. Other notable CAM options include Estlcam for simpler 2.5D work and Carbide Create for specific machine brands.
For machine control, GRBL-based controllers paired with software like Universal Gcode Sender (UGS) or Candle are prevalent for their open-source nature and affordability. Mach3 and LinuxCNC offer more advanced features and control over a wider range of hardware, often preferred by users seeking greater customization and industrial-level functionality.
Evaluating Metal Cutting Prowess
A hobby mill’s metal cutting ability is a composite of its rigidity, spindle power, and the precision of its motion system. While these machines excel at aluminum, brass, and plastics, their capacity for steel and harder alloys is more limited. Realistic expectations are key to avoiding frustration and achieving good results.
For aluminum, a well-tuned hobby mill can achieve depths of cut of 0.020-0.040 inches (0.5-1.0mm) per pass with a 1/4-inch end mill, maintaining good surface finish. Feeds and speeds must be carefully calculated to manage chip load and prevent tool breakage. Surface feet per minute (SFM) for aluminum typically ranges from 300-800, depending on the alloy and tool material.
Cutting mild steel requires significantly lighter passes, often in the range of 0.005-0.015 inches (0.12-0.38mm) depth of cut with a 1/4-inch end mill. SFM for mild steel is much lower, generally between 80-150, necessitating slower spindle speeds or smaller diameter tools. Achieving tight tolerances, such as +/- 0.002 inches (0.05mm), is possible on well-maintained hobby machines, but often requires multiple finishing passes and careful setup.
Here is a comparison of typical cutting parameters for a hobby milling machine: