
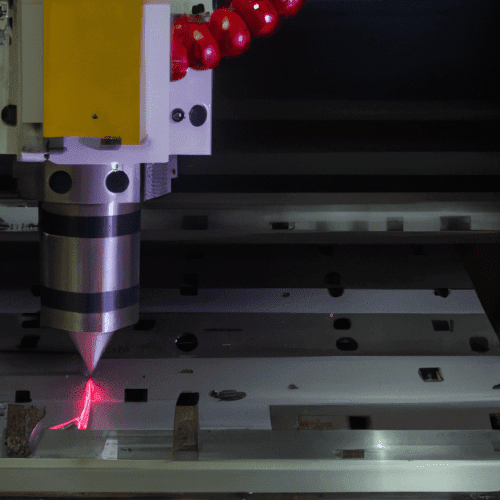
Selecting the appropriate laser wattage is a fundamental decision in CNC manufacturing, directly influencing material compatibility, cutting speed, edge quality, and overall production efficiency. Modern laser systems, encompassing diode, CO2, and fiber technologies, offer a broad spectrum of power outputs tailored for diverse applications and materials. Understanding the capabilities and limitations of each wattage range is essential for engineers and fabricators to achieve optimal results.
Understanding Laser Wattage and Its Impact
Laser wattage quantifies the power output of a laser cutting machine, serving as a primary determinant of its processing capabilities. Higher wattage systems can typically cut through thicker materials and achieve significantly faster cutting speeds. Conversely, lower power lasers are often better suited for delicate tasks requiring high precision or for engraving applications.
The interaction between laser power, material type, and thickness dictates the achievable cut quality and processing speed. Improper power settings can lead to issues such as incomplete cuts, excessive charring, or material damage due to overheating. Balancing these parameters is crucial for efficient and high-quality fabrication.
Modern laser cutters span a power range from approximately 30 watts up to 40,000 watts, or even 60,000 watts for extreme industrial applications. Lower-wattage systems typically handle thinner, non-metal materials, while higher-wattage machines are designed for fast, clean cuts on thicker metals.
Diode Lasers: Precision for Hobbyists and Light Engraving (5W-20W)
Diode laser engravers, commonly found in the 5W to 20W range, have gained immense popularity among hobbyists and small businesses due to their affordability and compact design. These systems typically operate with a blue-light laser, ideal for engraving and light cutting of non-metallic materials.
Applications for 5W-20W diode lasers include intricate engraving on wood, slate, leather, and anodized aluminum. They are also effective for cutting thin materials such as plywood (up to 6-10mm), pine, MDF, and certain dark-colored acrylics (3-5mm) in a single pass.
For cutting 3mm (1/8 inch) plywood, a 10W diode laser might operate at speeds between 8-15 mm/s for a single pass. Thicker materials like 6mm (1/4 inch) plywood often require two passes at slower speeds, typically 3-8 mm/s, to ensure a complete cut without excessive charring.
Engraving speeds for diode lasers generally range from 100-250 mm/s. While increasing power can proportionally increase speed, the mechanical rigidity of the gantry often limits the maximum effective speed for maintaining quality.
CO2 Lasers: Versatility for Organic Materials (40W-100W)
CO2 laser systems, typically ranging from 40W to 100W, are highly versatile for processing a wide array of organic and non-metallic materials. These machines are a staple in small workshops and signage production, offering a balance of power and precision.
Cutting wood is a primary application for CO2 lasers. A 40W system can cut 3-5mm wood, while 80W-100W machines are capable of cutting 8-12mm plywood, MDF, and softwood. For instance, an 80W CO2 laser can cut 3mm wood board at approximately 18 mm/s, increasing to 22 mm/s with a 100W system.
Acrylic cutting performance also scales with CO2 laser wattage. A 60W-100W laser can cut 3mm acrylic at 15-20 mm/s, 5mm acrylic at 7-10 mm/s, and 10mm acrylic at 2-3 mm/s. Cast acrylic generally yields better edge quality than extruded acrylic, which may require lower speeds or reduced power.
CO2 lasers are also highly effective for cutting and engraving other materials such as leather, cloth, paper, and rubber. Optimal settings for these materials vary significantly based on thickness and desired edge finish, often requiring careful tuning of speed, power, and air assist.
Industrial Fiber Lasers: Powering Metal Fabrication (1kW+)
Industrial fiber lasers, starting from 1kW and extending to tens of kilowatts, have revolutionized metal fabrication with their ability to cut a wide range of metals at high speeds and with exceptional precision. These solid-state lasers offer high energy efficiency and lower maintenance compared to older CO2 systems for metal.
A 1kW fiber laser is a robust entry-level industrial machine, capable of cutting mild steel up to 10mm (with oxygen assist) or 6-8mm (with nitrogen for clean edges). It can also handle stainless steel up to 6mm and aluminum up to 6mm, with brass and copper manageable on thinner sheets (typically <2-3mm).
As wattage increases, so does the cutting capacity and speed. A 3kW fiber laser can cut mild steel up to 16mm, stainless steel up to 8mm, and aluminum up to 6mm. Stepping up to 6kW allows for cutting mild steel up to 22mm, stainless steel up to 14mm, and aluminum up to 12mm.
For heavy plate production, 12kW systems can process carbon steel up to 40mm, stainless steel up to 30mm, and aluminum up to 18mm. Ultra-high-power lasers, such as 20kW and above, are capable of cutting carbon steel over 50mm and stainless steel over 40mm, catering to extreme thickness and productivity demands.
Cutting Speed, Thickness Capacity, and Tolerances
The relationship between laser wattage, cutting speed, and material thickness is critical for optimizing laser cutting operations. Generally, higher wattage enables faster cutting speeds and greater thickness capacity across all laser types. However, material properties, assist gas, and desired edge quality significantly influence these parameters.
For instance, a 6kW fiber laser can cut 1mm stainless steel at speeds up to 100-150 m/min. When cutting 3mm mild steel with oxygen assist, a 1kW fiber laser can achieve speeds of 15-20 m/min. These speeds decrease substantially as material thickness increases.
Standard laser cutting tolerances typically fall within ±0.1 mm to ±0.2 mm for linear dimensions under 100 mm, adhering to standards like DIN ISO 2768-1 m. Fiber lasers, especially high-end systems, can achieve tighter tolerances, sometimes reaching ±0.05 mm for thin metal sheets under optimal conditions.
For ultra-precision applications, such as aerospace or medical devices, advanced fiber laser systems can achieve tolerances as tight as ±0.0005 inches (±0.0127 mm). CO2 lasers, while precise for non-metals, generally have tolerances ranging from ±0.1 mm to ±0.5 mm.
Modern Engineering Practices and System Selection
Contemporary laser cutting systems integrate advanced optics, precision engineering, and sophisticated software controls to deliver remarkable accuracy and efficiency. These machines eliminate the need for physical cutting tools, reducing operating costs and material distortion.
Modern practices emphasize automation and artificial intelligence to optimize processes. Robotic material handling minimizes manual intervention, while AI-powered algorithms adjust cutting parameters in real-time, enhancing speed, reducing waste, and ensuring consistent quality. Predictive maintenance, driven by AI, also helps minimize downtime.
When selecting a laser system, engineers must consider the most common materials, maximum required thickness, desired cutting speed, and overall budget. Consulting validated thickness reference charts and equipment suppliers is crucial to pinpoint the appropriate wattage and technology for specific production needs.
The choice between diode, CO2, and fiber lasers depends heavily on the application. Diode lasers are excellent for hobbyist engraving and thin material cutting, CO2 lasers excel with a wide range of non-metals, and fiber lasers are the industry standard for high-speed, high-precision metal fabrication. Each technology offers distinct advantages for specific manufacturing challenges.