
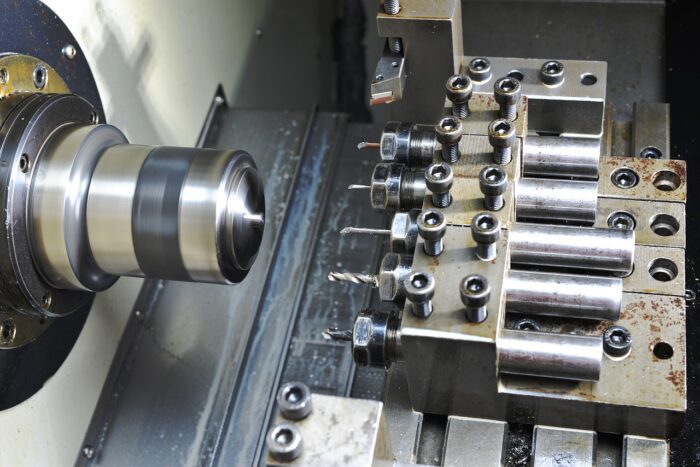
Precision machining demands meticulous attention to detail, where even minute deviations can compromise part integrity and functionality. Maintaining tight tolerances, often measured in microns or even sub-microns, requires a holistic approach encompassing environmental control, machine stability, and advanced tooling strategies.
Engineers and machinists striving for exceptional accuracy must consider every variable impacting the manufacturing process. From the ambient conditions of the workshop to the rigidity of the workholding, each element plays a critical role in achieving the desired dimensional precision.
Climate-Controlled Shop Environment
A stable shop environment is foundational for consistent precision machining. Temperature fluctuations directly cause thermal expansion and contraction in both machine tools and workpieces, leading to dimensional errors. Maintaining a consistent ambient temperature, typically 20°C (68°F) ±1°C, is paramount for high-accuracy operations.
Humidity control also impacts machine performance and material stability. High humidity can lead to corrosion of machine components and can affect certain workpiece materials. Conversely, extremely low humidity can increase static electricity, potentially interfering with sensitive electronic controls. Optimal relative humidity often falls within a 40-60% range.
Air quality is another significant factor. Airborne particulates, such as dust and coolant mist, can settle on machine ways, scales, and workpieces, introducing inaccuracies or premature wear. Implementing advanced air filtration systems, including HEPA filters, helps maintain a clean environment essential for ultra-precision work.
Machine Thermal Expansion Calibration
| Tolerance Grade | Description | Typical Application |
|---|---|---|
| Fine (f) | High precision, tight fits | Precision components, mating parts |
| Medium (m) | General machining, common fits | Standard engineering components |
| Coarse (c) | Less critical dimensions | Rough machining, non-functional surfaces |
| Very Coarse (v) | Rougher dimensions, large parts | Fabricated structures, large castings |
Even in a climate-controlled environment, machine tools generate heat during operation, causing thermal expansion of their structural components. This expansion can significantly shift the tool center point (TCP) relative to the workpiece, leading to dimensional errors. Modern CNC machines incorporate sophisticated thermal compensation systems to counteract these effects.
Regular calibration of these compensation models is essential. This involves using high-precision sensors to map the machine’s thermal behavior across its operating range and updating the control system’s algorithms. Some advanced machines utilize real-time temperature sensors embedded in critical components like the spindle and ball screws to dynamically adjust for thermal growth.
Preventative measures, such as allowing machines to warm up sufficiently before critical operations, also help stabilize thermal conditions. Consistent spindle warm-up routines ensure the spindle bearings and housing reach a stable operating temperature, minimizing thermal drift during machining cycles.
High-Quality Tooling
The quality of cutting tools directly dictates the achievable precision and surface finish. Using premium carbide grades, often with advanced coatings like TiAlN, AlCrN, or DLC, enhances tool life, reduces wear, and maintains sharp cutting edges for extended periods. These coatings improve lubricity and hardness, allowing for more aggressive feeds and speeds without compromising part quality.
Tool runout is a critical parameter; even a few microns of runout can significantly impact hole accuracy, surface finish, and tool life. High-precision tool holders, such as hydraulic chucks, shrink-fit holders, or high-precision collet chucks (e.g., ER-HP), are indispensable for minimizing runout to less than 3 microns (0.00012 inches). Balanced tool assemblies are also vital, especially for high-speed machining, to prevent vibration and maintain concentricity.
Selecting the correct tool geometry for the material and operation is equally important. For instance, end mills with specific helix angles and flute counts are optimized for different materials to ensure efficient chip evacuation and reduced cutting forces, both contributing to better dimensional control.
On-Machine Probe Inspection
Integrating on-machine probing capabilities significantly enhances precision by enabling in-process measurement and verification. Touch probes and laser tool setters allow for accurate workpiece setup, tool length measurement, and wear compensation directly within the machine’s work envelope. This eliminates the need to remove parts for inspection, reducing setup time and potential errors from re-fixturing.
In-process gauging with a touch probe can measure critical features after roughing or semi-finishing passes. The CNC control can then automatically adjust subsequent tool paths to compensate for any measured deviations, ensuring the final pass achieves the tightest possible tolerance. This adaptive machining approach is particularly valuable for complex geometries and high-value components.
Post-process inspection using the machine’s probe can verify final dimensions before the part leaves the machine. This provides immediate feedback on part quality and allows for rapid identification of any issues, preventing the production of out-of-spec parts. Probing systems typically offer repeatability in the sub-micron range, making them suitable for demanding applications.
Rigid Workholding
Workholding rigidity is fundamental to preventing workpiece deflection and vibration during machining, which are primary causes of dimensional inaccuracy and poor surface finish. The workholding system must securely clamp the part with sufficient force to resist cutting forces without deforming the workpiece itself.
Utilizing robust vises, hydraulic clamps, or custom fixtures designed for maximum stiffness is crucial. The clamping points should be strategically chosen to provide even pressure and support the workpiece near the cutting zone. For thin-walled or delicate parts, vacuum chucks or specialized low-deformation clamping solutions may be necessary to prevent distortion.
Vibration damping is another key aspect of rigid workholding. Incorporating materials with high damping characteristics, such as cast iron or specialized polymers, into fixture designs can absorb machining vibrations. Additionally, ensuring the workholding system is directly mounted to the machine table with minimal overhang further enhances overall rigidity and stability.