
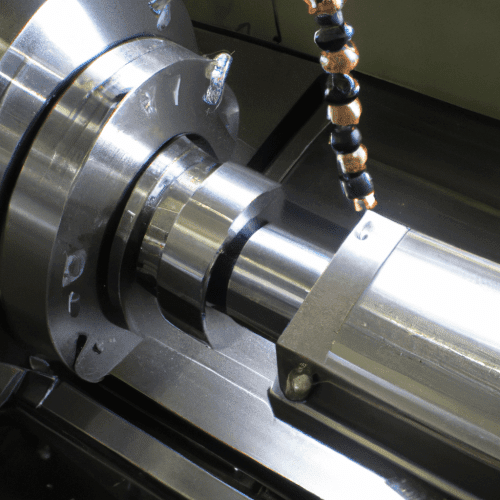
Precision manufacturing relies heavily on a diverse array of non-machining tooling, which underpins the accuracy, efficiency, and safety of CNC operations. These essential components, while not directly removing material, ensure workpieces are correctly positioned, measured, and prepared for the machining process. Their proper selection and application are critical for achieving tight tolerances and consistent part quality.
Effective non-machining tooling minimizes setup times, reduces human error, and prevents costly rework or machine damage. From securing raw stock to verifying finished dimensions, these tools are integral to a streamlined and productive CNC workflow. Understanding their functions and modern applications is fundamental for any tooling engineer.
Workholding Clamps, Vises, and Fixtures
Workholding clamps are fundamental devices that secure a workpiece to a machine bed or fixture, preventing movement and vibration during machining operations. Various types exist, including strap clamps, step clamps, toe clamps, and cam clamps, each suited for specific workpiece geometries and clamping requirements.
Strap clamps, often used with step blocks, provide versatile top-down clamping for flat workpieces, allowing height adjustment. Toe clamps offer low-profile side gripping, keeping the top surface clear for machining. Cam clamps provide quick-action mechanical clamping, ideal for rapid part changeovers in production environments.
Precision machine vises are robust workholding devices designed to hold workpieces securely for milling, drilling, and grinding. Modern vises are typically constructed from high-quality cast iron or hardened steel, ensuring rigidity and resistance to deflection under heavy cutting loads. Key specifications include jaw width, opening capacity, and critically, parallelism and squareness of the jaws. For production CNC work, parallelism and squareness should ideally be within 0.001 inch over the full jaw length and height.
Custom fixtures are engineered solutions tailored to specific parts, ensuring repeatable positioning and clamping for complex or high-volume production. These fixtures often integrate various clamping elements, such as hydraulic or pneumatic clamps, for consistent force and automated operation. Their design focuses on minimizing setup time and maximizing machining access while maintaining part integrity.
Magnetic Chucks
| Caliper Type | Typical Resolution | Typical Accuracy | Key Application |
|---|---|---|---|
| Digital Caliper | 0.0005″ (0.01 mm) | ±0.001″ (±0.02 mm) | General workshop, quick digital readout |
| Dial Caliper | 0.001″ (0.02 mm) | ±0.001″ (±0.02 mm) | Repeatable checks, visual feedback |
| Vernier Caliper | 0.001″ (0.02 mm) | ±0.001″ (±0.02 mm) | Basic measurement, no battery required |
Magnetic chucks provide an alternative workholding method, particularly advantageous for ferrous materials and applications requiring unobstructed access to multiple workpiece surfaces. These chucks utilize magnetic force to secure parts, eliminating the need for traditional mechanical clamps.
Three primary types of magnetic chucks are prevalent: permanent, electromagnetic, and electro-permanent. Permanent magnetic chucks use high-strength permanent magnets, offering consistent holding force without external power, making them energy-efficient and safe from power failures. However, their magnetic force is not adjustable, and they are less suitable for very heavy or non-magnetic workpieces.
Electromagnetic chucks generate magnetic force via an electric current, allowing for adjustable holding power and easy demagnetization. They are well-suited for precision machining and automated production, though they require a continuous power supply and may generate heat. Electro-permanent magnetic chucks combine the benefits of both, using an electrical pulse to activate or deactivate permanent magnets, providing strong, adjustable holding force without continuous power consumption.
Holding power for magnetic chucks is often measured in Newtons per square centimeter (N/cm²) or pounds per square inch (PSI). A fine pole magnetic chuck might offer around 100 N/cm² of holding force, while powerful electro-permanent chucks can reach 200 N/cm² or more for heavy-duty milling. Factors like workpiece thickness, surface finish, and material type significantly influence the actual holding force.
Measuring Calipers and Gauges
Precision measuring instruments are indispensable for verifying dimensions and ensuring quality control throughout the CNC manufacturing process. Calipers are versatile tools used for measuring external, internal, and depth dimensions. Digital calipers offer electronic readouts, often with resolutions down to 0.0005 inches (0.01 mm) and accuracy typically within ±0.001 inch (±0.02 mm). Dial and vernier calipers remain common for their reliability and cost-effectiveness.
Gauges encompass a broader range of specialized tools for specific measurement tasks. Height gauges, often used with granite surface plates, measure vertical distances and are crucial for setting tool heights and inspecting part features. Bore gauges are designed for accurate internal diameter measurements, detecting taper or out-of-round conditions in holes.
Thread gauges verify the accuracy of screw threads, ensuring proper fit and alignment for mating components. Gauge blocks, or ‘Jo blocks,’ are precision-ground steel or ceramic blocks used as master standards for calibrating other measuring instruments and setting machine offsets. These tools collectively ensure that machined parts adhere to specified tolerances, which for general CNC machining of metal parts is typically ±0.005 inches (±0.127 mm), with precision applications achieving ±0.001 inch (±0.025 mm) or tighter.
Tool Setters
Tool setters are high-precision sensors integrated into CNC machines to automate the measurement of cutting tool length and diameter offsets. This automation significantly reduces setup time, improves accuracy, and prevents potential machining defects.
Two main types of tool setters are widely used: contact and non-contact. Contact tool setters, also known as touch-trigger probes, physically contact the tool’s cutting edge to determine its position. They offer high repeatability, often better than 1.0 µm (2σ), and are robust in harsh machining environments.
Non-contact tool setters, primarily laser-based systems, use a laser beam to measure tool dimensions without physical contact. This method is particularly beneficial for delicate tools, small-diameter tools (down to 0.03 mm), and high-speed measurement, preventing wear or damage to the tool. Modern laser setters can achieve repeatability as fine as ±0.1 µm (2σ).
Integrating tool setters into CNC systems allows for automatic updating of tool offsets, real-time monitoring of tool wear and breakage, and compensation for thermal deformation of the machine spindle. This capability is crucial for maintaining consistent part quality in automated and high-precision machining operations, ultimately reducing scrap and increasing productivity.