
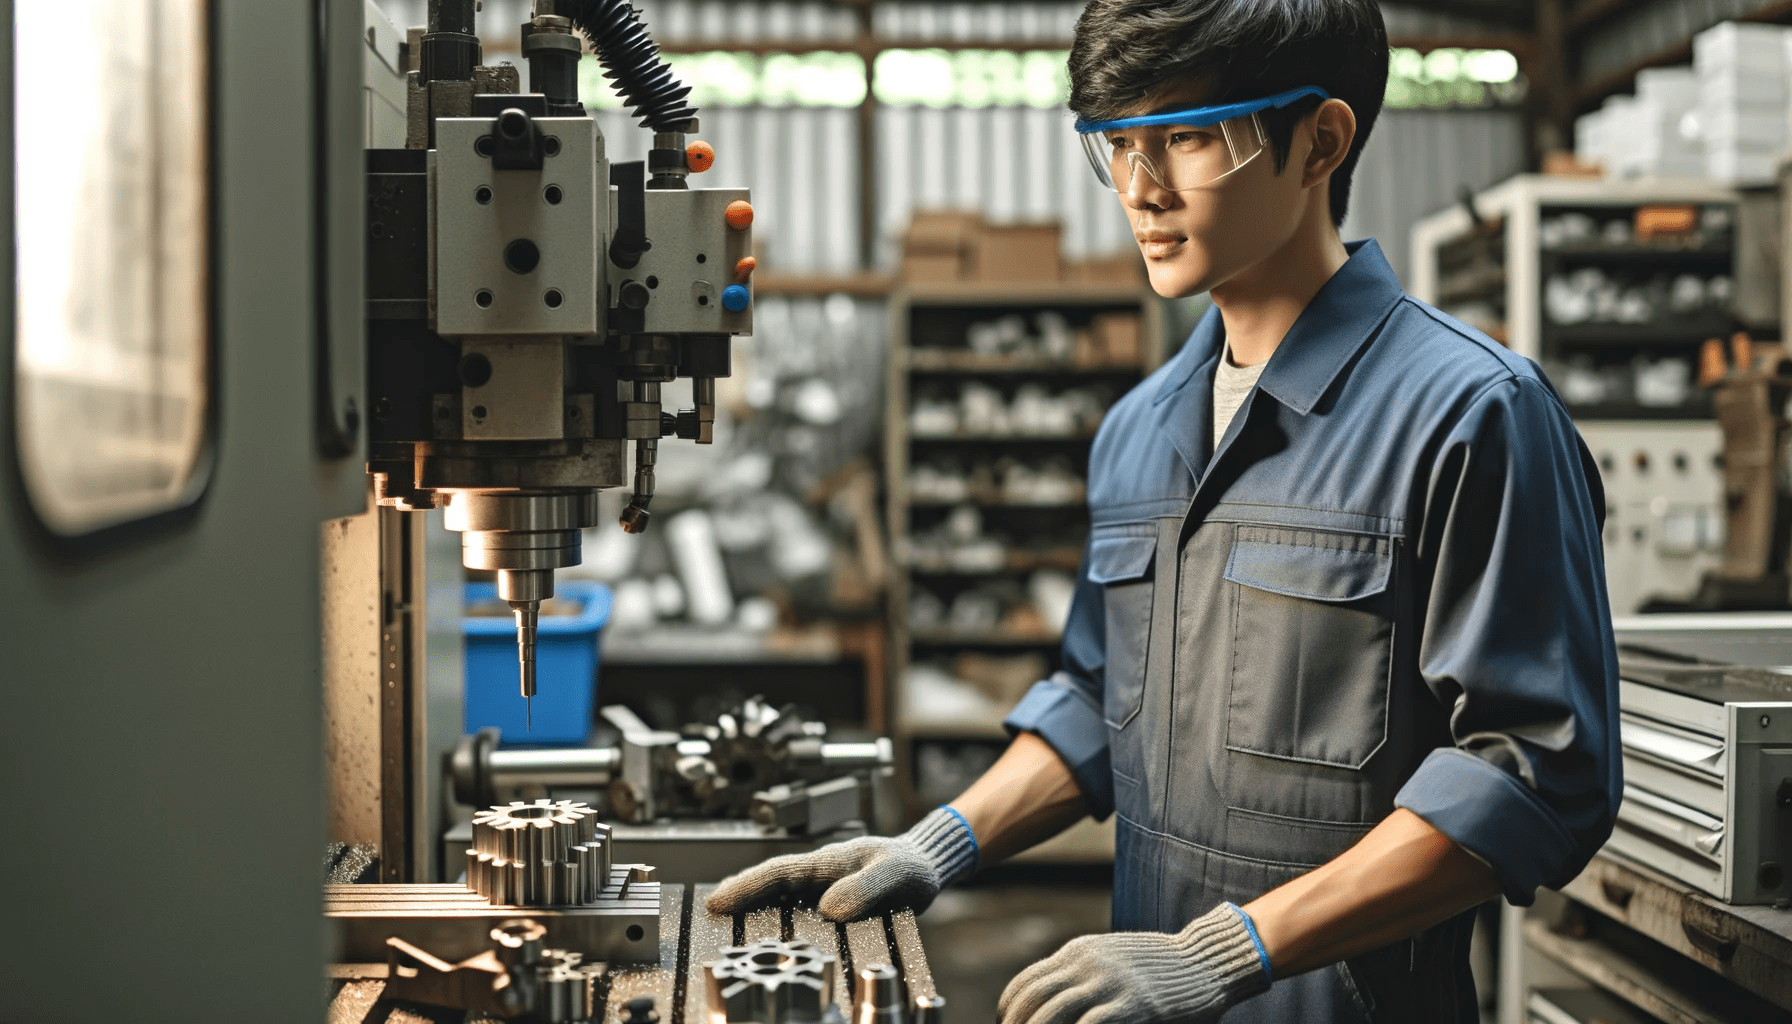
High-speed CNC machining fundamentally transforms material removal rates and surface finish quality. Modern machine tools leverage advanced kinematics and control systems to push boundaries previously considered unattainable.
Precision Spindle Dynamics
Maintaining exceptional spindle balance is paramount for achieving optimal performance and longevity in high-speed machining operations. Unbalanced spindles generate excessive vibration, leading to premature bearing wear, poor surface finishes, and reduced tool life.
ISO 1940-1 specifies balance quality requirements for rigid rotors, with G-class ratings often applied to high-speed spindles. For precision applications, a balance grade of G0.4 or G1.0 is frequently targeted, ensuring minimal vibration at operational speeds and extending the lifespan of critical components. This stringent standard helps prevent resonant frequencies that can degrade machining quality.
Advanced balancing techniques, including dynamic balancing at operating speeds, are critical for spindles exceeding 20,000 RPM. These methods compensate for mass distribution irregularities across multiple planes, significantly reducing dynamic runout and ensuring smooth, stable rotation even under extreme centrifugal forces. Such precision balancing is essential for achieving tight tolerances and improved energy efficiency.
Spindle bearings, often ceramic hybrid types, play a crucial role in high-speed stability. Their lower density and higher stiffness compared to steel bearings allow for higher rotational speeds with less heat generation and improved rigidity. This translates to superior damping characteristics and extended service intervals, which are vital for continuous high-performance operation.
Optimized Cutting Tool Geometries
| Parameter | High-Speed Machining (HSM) | Conventional Machining |
|---|---|---|
| Spindle Speed (RPM) | > 15,000 (often 20,000 – 90,000+) | < 10,000 |
| Feed Rate (mm/min) | > 5,000 (often 10,000 – 30,000+) | < 2,000 |
| Linear Motor Acceleration | Up to 12G or more | Typically < 0.5G (ball screw) |
| Surface Finish (Ra) | < 0.4 µm | 0.8 – 3.2 µm |
| Positional Accuracy | ± 2 µm | ± 5 – 10 µm |
High-feed end mills are engineered with specific geometries to maximize material removal rates while managing cutting forces. Their unique design typically features a shallow lead angle, which thins the chip axially rather than radially.
This chip thinning effect allows for significantly higher feed rates compared to conventional end mills, distributing cutting forces over a larger area of the cutting edge. This reduces heat generation at the tool tip and minimizes tool wear, leading to improved tool life and reduced cycle times.
Modern high-feed tools often incorporate multiple flutes and advanced coatings like AlTiN or AlCrN, which enhance hardness, lubricity, and thermal stability. These coatings are essential for resisting the extreme temperatures encountered during aggressive high-speed milling, extending tool life, and improving surface finish.
Tool runout is another critical factor; even slight deviations can drastically impact tool life and surface finish. Precision tool holders, such as hydraulic or shrink-fit systems, are essential for maintaining concentricity and rigidity, ensuring consistent chip loads and preventing premature tool failure.
Linear Motor Drive Systems
Rapid acceleration linear motors are fundamental to achieving the dynamic performance required in high-speed CNC. Unlike traditional ball screw systems, linear motors directly convert electrical energy into linear motion, eliminating mechanical backlash and friction.
These direct-drive systems offer superior acceleration and deceleration capabilities, often exceeding 1G (9.8 m/s²) in modern machines, with some reaching up to 12G for specific applications. This allows for faster contouring and reduced non-cutting times, significantly boosting overall productivity and cycle time reduction.
Positioning accuracy with linear motors is exceptionally high, often within micrometers, due to the absence of mechanical wear components. Integrated linear encoders provide real-time feedback, ensuring precise control over tool path execution and correcting for potential errors from mechanical linkages.
The stiffness of linear motor drives also contributes to improved surface finish and dimensional accuracy. Their ability to respond instantaneously to control signals minimizes overshoot and vibration during rapid direction changes, which is crucial for maintaining tight tolerances.
Advanced Motion Control Algorithms
Dynamic motion control systems are the brain behind high-speed machining, orchestrating complex tool paths with precision and speed. Look-ahead control is a core component, analyzing upcoming G-code blocks to anticipate machine movements.
This predictive capability allows the controller to smoothly accelerate and decelerate the machine axes, maintaining optimal feed rates through complex geometries. It prevents abrupt changes that could induce vibration or compromise surface quality, leading to smoother cornering and consistent feed rates.
Jerk control, which manages the rate of change of acceleration, is another vital algorithm. By limiting sudden changes in acceleration, jerk control minimizes mechanical shock and resonance, extending machine life, improving part accuracy, and preventing chatter marks on the surface finish.
Adaptive control systems further enhance performance by monitoring real-time cutting conditions, such as spindle load, vibration, and temperature. These systems can dynamically adjust feeds and speeds to optimize material removal, prevent tool breakage, and ensure higher part accuracy.
Thermal Management Strategies
Effective heat dissipation is crucial in high-speed CNC machining to maintain dimensional accuracy and extend component life. Significant heat is generated from both the cutting process and the machine’s internal components, particularly the spindle and linear motors.
Spindle cooling systems often employ chilled water or oil circulation through internal channels to regulate bearing and motor temperatures. Maintaining a stable spindle temperature prevents thermal expansion that could lead to runout and accuracy issues, ensuring consistent performance.
Coolant delivery methods have evolved beyond simple flood cooling. High-pressure through-spindle coolant and minimum quantity lubrication (MQL) systems efficiently remove heat from the cutting zone, evacuate chips, and provide lubrication, which is critical for tool life in high-speed operations.
Thermal compensation software actively monitors temperature sensors throughout the machine structure. It then applies real-time adjustments to axis positions, counteracting thermal expansion or contraction and ensuring consistent part dimensions, especially during long machining cycles.