
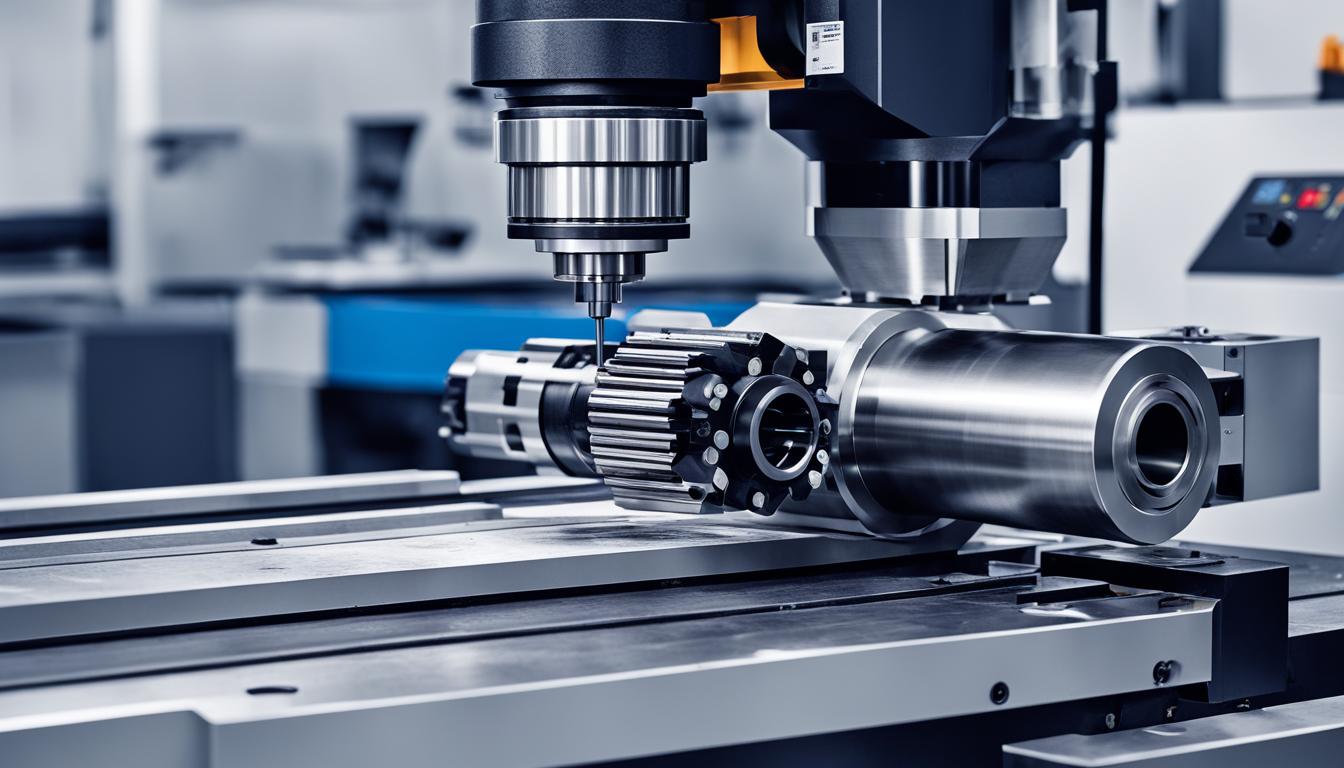
A machining center represents an advanced Computer Numerical Control (CNC) machine tool, integrating multiple machining operations such as milling, drilling, tapping, and boring into a single, automated platform. These sophisticated systems are fundamental to modern production facilities, enhancing both efficiency and the precision of manufactured products.
The core distinction of a machining center lies in its ability to automatically change tools during the machining process, eliminating manual intervention. This capability, facilitated by an automatic tool changer (ATC) and a tool magazine, allows for complex, multi-step operations to be completed efficiently.
Enclosed Multi-Axis Machine Tool Systems
Enclosed multi-axis machine tools provide a controlled environment for precision manufacturing, safeguarding operators from chips, coolant, and moving components. These enclosures also help maintain thermal stability, which is crucial for achieving tight tolerances in demanding applications.
Multi-axis machining centers, typically featuring 4, 5, or even up to 9 axes, significantly expand geometric capabilities beyond traditional 3-axis machines. This allows for cutting from multiple angles in a single setup, reducing the need for manual repositioning and minimizing potential errors.
The added axes enable the cutting tool to approach the workpiece from various orientations, facilitating the creation of intricate shapes, contours, and undercuts. This flexibility improves surface finish quality, optimizes chip evacuation, and extends tool life by allowing for more efficient tool angles.
Automatic Tool Changers and CNC Control Integration
| Factor | Vertical Machining Center (VMC) | Horizontal Machining Center (HMC) |
|---|---|---|
| Spindle Orientation | Vertical | Horizontal |
| Best For | General machining, lower volume, simpler setups | High volume, multi-face parts, heavier cutting |
| Operator Access | Typically easier | Can be less direct, depending on fixturing |
| Chip Evacuation | Can collect on workpiece | Usually better, gravity-assisted |
| Floor Space | Generally less | Often more |
| Initial Cost | Usually lower | Usually higher |
Automatic Tool Changers (ATCs) are indispensable components of modern machining centers, enabling rapid and automated tool exchanges without operator intervention. This mechanism dramatically reduces non-productive time and supports complex machining tasks requiring numerous tools.
An ATC system operates through servo-driven or pneumatic mechanisms, precisely coordinating the removal of the current tool and the insertion of the next from a tool magazine. This automated sequence, controlled by the CNC program, ensures seamless transitions and maintains machining precision.
CNC control systems serve as the ‘brain’ of the machining center, interpreting G-code programs and translating them into precise axis movements and spindle operations. Major control platforms like Fanuc, Siemens Sinumerik, and Haas offer varying features, programming interfaces, and integration capabilities.
Integration between the CNC controller and auxiliary Programmable Logic Controllers (PLCs) is critical for managing machine functions beyond motion control. PLCs handle tasks such as tool changer sequencing, coolant management, chip conveyors, and safety interlocks, allowing the CNC to focus on precise tool path execution.
Vertical versus Horizontal Orientation
Machining centers are primarily categorized by their spindle orientation: vertical or horizontal. Each configuration offers distinct advantages tailored to specific part geometries, production volumes, and material removal requirements.
Vertical Machining Centers (VMCs) feature a vertically oriented spindle, with the cutting tool approaching the workpiece from above. VMCs are often preferred for general machining, lower-volume work, and simpler setups due to easier operator access and visibility into the work area.
Horizontal Machining Centers (HMCs) utilize a horizontally oriented spindle, allowing the tool to approach the part from the side. HMCs excel in high-volume production, multi-face machining, and heavier chip loads, often paired with tombstones or pallet changers for enhanced efficiency.
Chip evacuation is a significant differentiator; in VMCs, chips can accumulate on the workpiece, potentially interfering with the cut. HMCs benefit from gravity-assisted chip fall, which helps clear the work zone, supporting higher throughput and longer unattended runs.
High-Precision Component Fabrication
High-precision component fabrication relies on machining centers to produce parts with extremely tight dimensional tolerances and consistent repeatability. Industries such as aerospace, medical, and automotive demand this level of accuracy for critical components.
Precision in CNC manufacturing is measured by tolerance, surface finish, and repeatability. Standard machining tolerances often range from ±0.05 mm to ±0.13 mm for many metal parts, but precision applications can require tolerances as tight as ±0.005 mm on critical features.
Achieving optimal tolerances involves meticulous control over various factors, including machine rigidity, spindle runout, tooling, workholding, thermal stability, and cutting parameters. Advanced CNC equipment precisely controls speed, feed rate, and tool positioning to maintain consistency.
Feeds and speeds are critical parameters influencing precision and surface finish. For instance, aluminum typically uses cutting speeds of 200-400 m/min and feed rates of 300-500 mm/min, while titanium requires slower speeds of 30-70 m/min and feed rates of 80-150 mm/min.
Repeatability, the machine’s ability to consistently return to the same position over multiple attempts, is often considered more critical than absolute accuracy for stable production. Even with slight positioning errors, excellent repeatability allows for compensation to maintain machining consistency.