
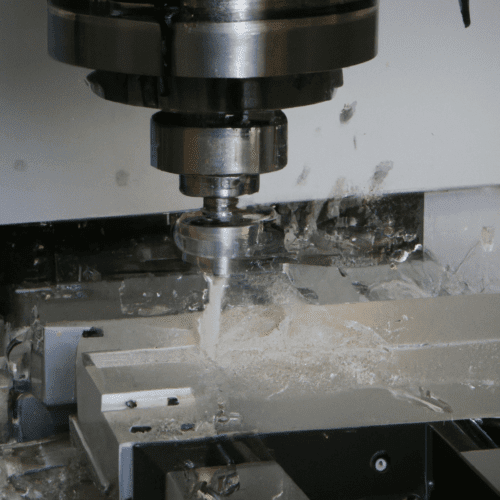
Milling operations form the bedrock of subtractive manufacturing, shaping raw material into precise components. Two primary methodologies dominate this field: Computer Numerical Control (CNC) milling and conventional (manual) milling. While both achieve material removal, their operational philosophies, capabilities, and economic implications diverge significantly.
Understanding these differences is crucial for engineers and manufacturers selecting the optimal process for specific production requirements. Modern manufacturing increasingly leans towards automation, yet conventional methods retain niche applications where their unique characteristics are advantageous.
Fundamental Operational Principles
CNC milling relies on pre-programmed computer software to automate and precisely guide machine tools, executing complex toolpaths with minimal human intervention. This digital control system, often involving CAD/CAM software, translates design specifications into G-code, which dictates every movement of the cutting tool.
Conventional milling, conversely, depends on direct human control. Operators manipulate handwheels and levers to move the workpiece or the cutting tool along the X, Y, and Z axes. This manual operation demands significant skill and continuous attention from the machinist to achieve desired geometries and surface finishes.
Automated toolpath execution is a hallmark of CNC systems, where CAM software generates optimized cutting paths based on part geometry, material properties, and machining strategies. This automation drastically reduces programming time and minimizes human error in toolpath design.
Advanced CAM software, sometimes augmented with AI, can generate toolpaths in minutes by holistically analyzing the setup and evaluating multiple machining strategies. This allows for rapid, safe programming and consistent machine behavior across various parts.
Precision, Complexity, and Automation
| Parameter | CNC Milling | Conventional Milling |
|---|---|---|
| Operational Control | Automated (G-code, CAM software) | Manual (handwheels, levers) |
| Toolpath Complexity | Complex 3D contours, multi-axis | Simple 2D features, limited contours |
| Precision/Tolerance | ±0.05 mm to ±0.13 mm (standard), up to ±0.005 mm (precision) | ±0.1 mm to ±0.2 mm (general), tighter with high skill |
| Production Speed | High volume, continuous, fast | Low volume, slower, operator-dependent |
| Initial Investment | $15,000 – $500,000+ (professional to industrial) | Often under $10,000 (basic models) |
| Feeds & Speeds (Aluminum) | RPM: 8,000-20,000+, Feed: 40-150 IPM | RPM: 500-8,000, Feed: Lower, operator-dependent |
| Feeds & Speeds (Steel) | RPM: 1,900-6,000+, Feed: 7-200 IPM | RPM: 500-8,000, Feed: Lower, operator-dependent |
Complex 3D contouring capability is a significant differentiator, with CNC milling excelling in this domain. Multi-axis CNC machines, particularly 5-axis systems, can position the cutting tool at virtually any angle, enabling the creation of intricate features, freeform surfaces, and complex geometries in a single setup.
Contour milling, a specialized CNC technique, involves continuous cutting along a part’s outer contour or spatial surface, making it ideal for high-precision curved structures required in aerospace or mold making. This method achieves high accuracy and uniformity along complicated shapes that are unattainable with simpler milling operations.
Conventional milling is largely limited to simpler 2D features, such as flat surfaces, slots, and basic pockets. Achieving even moderately complex contours manually is exceptionally challenging, time-consuming, and often requires multiple setups and highly experienced operators. The inherent limitations of manual control restrict the geometric complexity that can be reliably produced.
Standard CNC machining tolerances typically range from ±0.05 mm to ±0.13 mm for most milling operations. For precision applications, tolerances as tight as ±0.01 mm are achievable with careful process control, proper tooling, and experienced operators.
Conventional milling generally yields looser tolerances, often in the range of ±0.1 mm to ±0.2 mm for general dimensions. Achieving tighter tolerances manually is possible but demands exceptional operator skill and often involves more time-consuming, iterative adjustments.
Production Efficiency and Throughput
Production batch speed is where CNC milling demonstrates a clear advantage. Modern CNC systems are engineered for high production capacity, operating continuously for 24 hours a day without breaks. This capability significantly reduces lead times and enables rapid, efficient production of large batches.
The automated and repeatable nature of CNC machining ensures consistent quality across thousands of identical parts, minimizing errors and waste. High-speed CNC milling techniques further boost efficiency by employing high spindle speeds and feed rates, leading to faster material removal rates and reduced cycle times.
Conventional milling, being a manual process, is inherently slower and less consistent for batch production. Each part requires individual operator attention, leading to variations between pieces and making high-volume production impractical. It is best suited for one-off parts, prototyping, or repair work where speed is not the primary concern.
Efficiency in CNC machining also translates to lower labor costs per part and optimized material utilization, as machines can run unattended for extended periods. This contrasts sharply with conventional milling, which requires constant operator presence and oversight.
Investment and Operational Considerations
The initial investment difference between CNC and conventional milling machines is substantial. New industrial CNC machining centers can range from $50,000 for entry-level vertical machining centers to over $500,000 for high-end 5-axis or multi-tasking platforms. Professional shop machines typically fall between $15,000 and $30,000.
Entry-level CNC vertical machining centers (VMCs) in 2026 start around $35,000 to $65,000, suitable for prototyping and light repair. Mid-range workhorse VMCs, ideal for general job shops, cost between $70,000 and $145,000.
Conventional milling machines, by contrast, represent a significantly lower initial capital outlay. New manual mills can often be acquired for under $10,000, making them accessible for hobbyists, small workshops, or educational institutions with limited budgets. Used conventional machines are even more affordable.
Beyond the machine itself, CNC operations require additional investments in CAD/CAM software, tooling, workholding, and operator training. These supplementary costs can add 20-30% to the machine’s purchase price.
Modern Machining Parameters and Tolerances
Modern CNC milling utilizes precise feeds and speeds tailored to specific materials and tooling. For aluminum (6061), typical CNC spindle speeds range from 8,000 to 20,000+ RPM, with feed rates between 40 and 150 inches per minute (IPM).
Steel (e.g., 1018 or 4140) requires different parameters, with CNC spindle speeds often between 1,900 and 6,000 RPM and feed rates from 7 to 200 IPM, depending on the specific alloy and operation. Carbide tooling is standard for these applications.
Conventional milling typically operates at much lower spindle speeds and feed rates, often in the range of 500 to 8,000 RPM for general operations, with feed rates determined by operator feel and material response. This slower pace is necessary due to the lack of automated feedback and the need for manual control.
Achievable tolerances are a critical performance metric. While standard CNC machining can hold ±0.13 mm (±0.005″) for most operations, precision applications can reach ±0.01 mm (±0.0004″) or even ±0.005 mm (±0.0002″) for critical features under controlled conditions.