
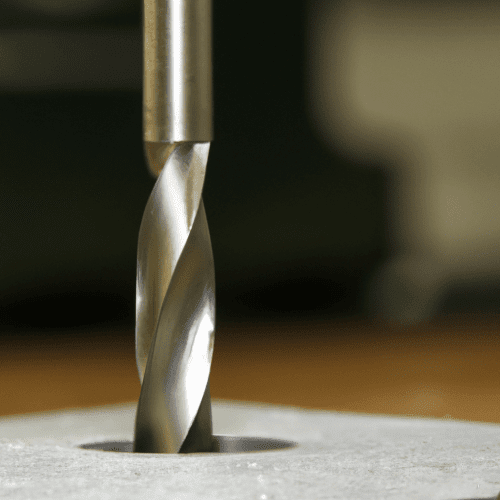
Achieving precise and clean cuts in hardwood milling demands a strategic approach to tooling and machining parameters. The selection of the appropriate end mill, coupled with careful adjustments to feed rates and an understanding of wood grain orientation, significantly impacts the final product’s quality and tool longevity.
This technical guide explores the critical aspects of utilizing two-flute spiral downcut end mills, the benefits of carbide tooling, precise feed rate adjustments, and essential considerations for navigating diverse wood grain patterns.
Two-Flute Spiral End Mills
Two-flute spiral end mills are a common choice for woodworking applications, particularly for their ability to efficiently remove material. The helical flutes on these cutters are designed to lift or push chips, depending on their orientation, facilitating material evacuation from the cutting zone.
These tools are versatile for various operations, including roughing and plunge cutting in softwoods and plywood. The larger flute spaces inherent in two-flute designs help prevent clogging, especially when machining resinous woods.
Downcut Bits for Clean Edges
Downcut spiral end mills are specifically engineered to produce exceptionally clean top edges on workpieces by pushing wood chips and fibers downward into the cut. This action effectively minimizes splintering and tear-out on the top surface, which is crucial for finished faces and delicate materials like veneers or laminated plywood.
While downcut bits excel at surface finish, their chip evacuation can be less efficient than upcut tools, especially in deep slots or pockets, potentially leading to chip packing and increased heat. To mitigate this, a slower feed rate and lighter depth of cut are often recommended.
Carbide Tipped Cutters
Carbide end mills, whether solid carbide or carbide-tipped, offer superior performance in hardwood milling due to their exceptional hardness, wear resistance, and heat resistance. These properties allow them to maintain a sharp edge significantly longer than high-speed steel (HSS) alternatives, reducing the frequency of tool changes and overall downtime.
Solid carbide end mills are particularly tough and long-lasting, making them ideal for cutting dense and abrasive hardwoods, as well as engineered wood products. While the initial investment for carbide tools can be higher, their extended lifespan and consistent cutting precision often result in long-term cost-effectiveness.
Feed Rate Adjustments
Optimizing feed rate is paramount for achieving desired surface finish and maximizing tool life in hardwood milling. Chip load, defined as the amount of material removed by each cutting edge per revolution, is a critical factor in determining the appropriate feed rate.
The formula for calculating feed rate (F) is: F (IPM) = RPM × Number of Flutes × Chip Load (inches per tooth). For dense hardwoods like walnut, a typical 2-flute end mill might use a chip load of 0.002–0.004 inches, with RPMs ranging from 6,000–8,000 and feed rates between 60–100 IPM. Conversely, too slow a feed rate can cause rubbing and excessive heat, leading to burning and premature tool wear, especially in hardwoods.
Grain Orientation Considerations
Wood is an anisotropic material, meaning its properties vary depending on the direction of the grain. Understanding grain orientation is crucial for minimizing tear-out and achieving a clean finish. Cutting perpendicular to the grain, often referred to as ‘across the grain,’ generally results in larger cutting forces.
Whenever possible, orienting the toolpath to cut ‘with the grain’ rather than ‘against it’ significantly reduces the risk of fiber separation and tear-out. When cutting end grain, which is particularly prone to tear-out, using very sharp tools and taking lighter passes can improve results. Performing end grain cuts before long grain cuts can also help manage tear-out.
| Parameter | Two-Flute Downcut Carbide End Mill (Hardwood) | Two-Flute Upcut Carbide End Mill (Hardwood) |
|---|---|---|
| Primary Benefit | Clean top surface, reduced tear-out | Efficient chip evacuation, good for deep cuts |
| Chip Evacuation | Pushes chips downward, can lead to packing in deep cuts | Pulls chips upward, clears cutting path |
| Surface Finish (Top) | Excellent, minimal splintering | Potential for tear-out on top surface |
| Surface Finish (Bottom) | May have slight burr if cutting through | Clean bottom surface |
| Recommended Feed Rate | Slower, lighter depth of cut often preferred | Can generally use higher feed rates |
| Typical Chip Load (Hardwood) | 0.002–0.004 inches per tooth | 0.002–0.004 inches per tooth (similar starting point) |
| Standard Tolerance (CNC Wood) | ±0.2 mm for CNC-routed parts | ±0.2 mm for CNC-routed parts |