
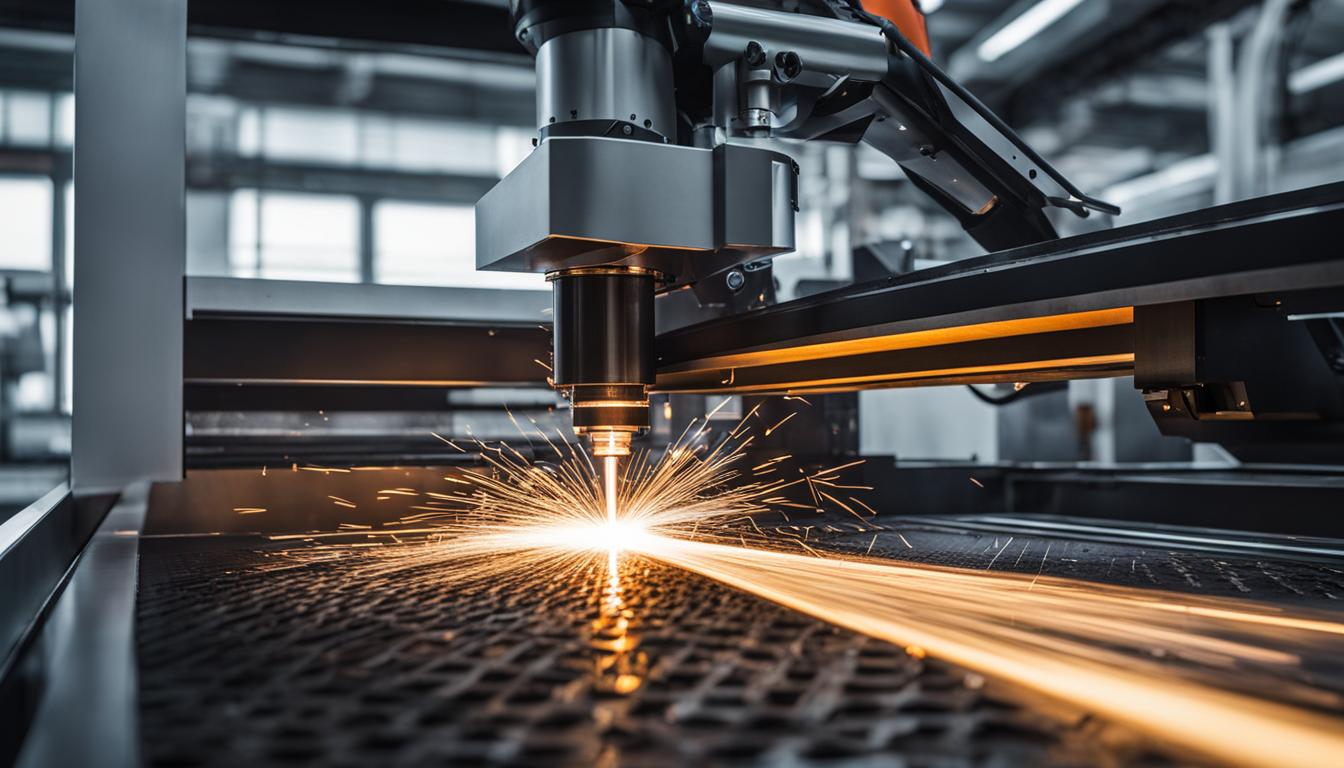
Computer Numerical Control (CNC) laser cutting has become a foundational technology in modern manufacturing, offering unparalleled precision and efficiency across diverse industries. This non-contact thermal process utilizes a highly concentrated beam of light to melt, vaporize, or burn material along a programmed path. Its versatility allows for intricate designs and high-quality finishes on a wide array of materials.
Focused Laser Beam Cutting Principles
The core of any CNC laser system is its ability to generate and precisely focus a high-energy light beam. This beam, originating from a laser source, is directed through a series of mirrors and lenses within the cutting head. The optical system converges the laser energy into an extremely small spot, typically with a diameter as fine as a few microns, at the material’s surface.
This concentrated energy rapidly heats the material, causing it to melt, vaporize, or burn away. The resulting narrow channel, known as the ‘kerf,’ is the width of the material removed during the cut. Typical laser cutting kerf widths range from 0.08 mm to 1 mm, influenced by factors like laser type, material, and thickness. Fiber lasers generally produce a tighter kerf (0.15–0.5 mm) compared to CO2 lasers (0.25–0.5 mm).
Precision CNC Gantry Positioning
| Parameter | CO2 Laser | Fiber Laser |
|---|---|---|
| Laser Medium | Gas mixture (CO2, N2, He) | Solid-state optical fibers |
| Wavelength | 10.6 µm | 1.06 µm |
| Typical Power Range | 30W – 4000W | 500W – 40,000W |
| Primary Materials | Acrylic, wood, plastics, paper, leather, some thin metals | Metals (stainless steel, carbon steel, aluminum, copper, brass) |
| Energy Efficiency | ~30% | >45% |
| Maintenance | Higher (tube replacement) | Lower (solid-state design) |
| Kerf Width (typical) | 0.25 mm – 0.5 mm | 0.15 mm – 0.5 mm |
Achieving accurate cuts requires a sophisticated motion control system, typically a CNC gantry. This gantry precisely moves the laser cutting head across the workpiece in X, Y, and sometimes Z axes, following the digital design file. Modern gantry systems ensure high positional accuracy, often reaching ±0.1 mm, with repeatability as tight as ±0.03 mm.
The integration of advanced software and artificial intelligence further enhances gantry performance. AI-powered optimization can adjust cutting parameters in real-time, improving speed, reducing waste, and ensuring consistent quality. This level of control is crucial for producing complex geometries and maintaining tight tolerances across production runs.
CO2 versus Fiber Laser Sources
Two primary laser technologies dominate the industrial cutting landscape: CO2 and fiber lasers. Each operates on distinct principles and offers specific advantages for different materials and applications. Fiber lasers have become the leading technology, accounting for over 60% of global installations by 2025, due to their efficiency and speed.
CO2 lasers utilize a gas mixture, primarily carbon dioxide, electrically stimulated to produce a laser beam with a wavelength around 10.6 µm. These lasers are highly effective for processing non-metallic materials such as wood, acrylic, plastics, paper, leather, and some thin metals. Their power ranges typically from 30 to 4000 watts, with industrial systems often between 40W and 300W for non-metals.
Fiber lasers, conversely, use solid-state technology where the laser beam is generated by banks of diodes and channeled through optical fibers. They operate at a much shorter wavelength, around 1.06 µm, making them highly efficient for cutting reflective metals like stainless steel, carbon steel, aluminum, copper, and brass. Fiber laser power ranges are significantly higher, from 500 to 40,000 watts, with many industrial systems in the 1 kW to 15 kW range.
Fiber lasers boast higher energy efficiency, exceeding 45% wall-plug efficiency compared to CO2 lasers’ 30%. This translates to lower operating costs and faster cutting speeds, up to 30% quicker for thin metals. While CO2 lasers require regular maintenance and tube replacement, fiber lasers have a solid-state design with fewer moving parts, leading to minimal maintenance and reduced downtime.
Achieving Clean Edge Metal and Acrylic Cutting
Producing clean, high-quality edges is a hallmark of effective laser cutting. This is largely influenced by precise control over laser parameters and the strategic use of assist gases. The laser beam melts or vaporizes the material, and an assist gas is then directed into the cut zone to expel molten material and prevent re-solidification.
Oxygen is a common assist gas for cutting carbon steel and other ferrous materials. It reacts exothermically with the metal, generating additional heat that accelerates the cutting process. However, this reaction can lead to oxidized, rougher edges that may require post-processing.
Nitrogen, an inert gas, is preferred for stainless steel, aluminum, and other non-ferrous metals. It creates a non-reactive environment, preventing oxidation and resulting in clean, oxide-free cuts with superior edge quality. Compressed air can also be used for less critical applications, offering a balance of cost and performance.
Acrylic cutting with CO2 lasers often yields a ‘flame-polished’ edge, a smooth, glossy finish directly from the machine. This is achieved by carefully balancing power and speed settings, typically using maximum power at the highest safe speed to prevent excessive melting and bubbling. For a 150W CO2 laser cutting 3mm acrylic, speeds of 25-40 mm/s at 35-55% power are common starting points.
Non-Contact Sheet Processing Advantages
Laser cutting is inherently a non-contact process, meaning the cutting tool (the laser beam) never physically touches the workpiece. This fundamental characteristic offers significant advantages over traditional contact-based cutting methods like milling or punching. There is no mechanical stress or deformation induced in the material, preserving its integrity.
The absence of physical contact eliminates tool wear, reducing operational costs and downtime associated with tool changes and sharpening. This also allows for cutting extremely intricate geometries and delicate materials without the risk of tearing or distortion. Parts fabricated this way often require minimal secondary processing, saving time and resources.
Non-contact processing also contributes to the high precision and repeatability of CNC laser systems. With no physical forces acting on the material, the gantry system can maintain its programmed path with exceptional accuracy. This ensures consistent part quality across large production batches, a critical factor in industries demanding tight tolerances.
For a 1kW fiber laser cutting 3mm mild steel, typical speeds can be quite fast, often in the range of several meters per minute, depending on the specific alloy and assist gas. For example, a 1000W fiber laser can cut up to 10mm carbon steel. CO2 lasers cutting 6mm acrylic might operate around 1200 mm/min with appropriate power settings.
Standard laser cutting tolerances generally fall within ±0.1 mm to ±0.2 mm for linear dimensions under 100 mm. For critical features like small holes, modern fiber lasers can achieve precision capabilities of ±0.05 mm, and even ±0.0127 mm under optimal conditions. These tight tolerances are crucial for precision components in aerospace and medical device manufacturing.