
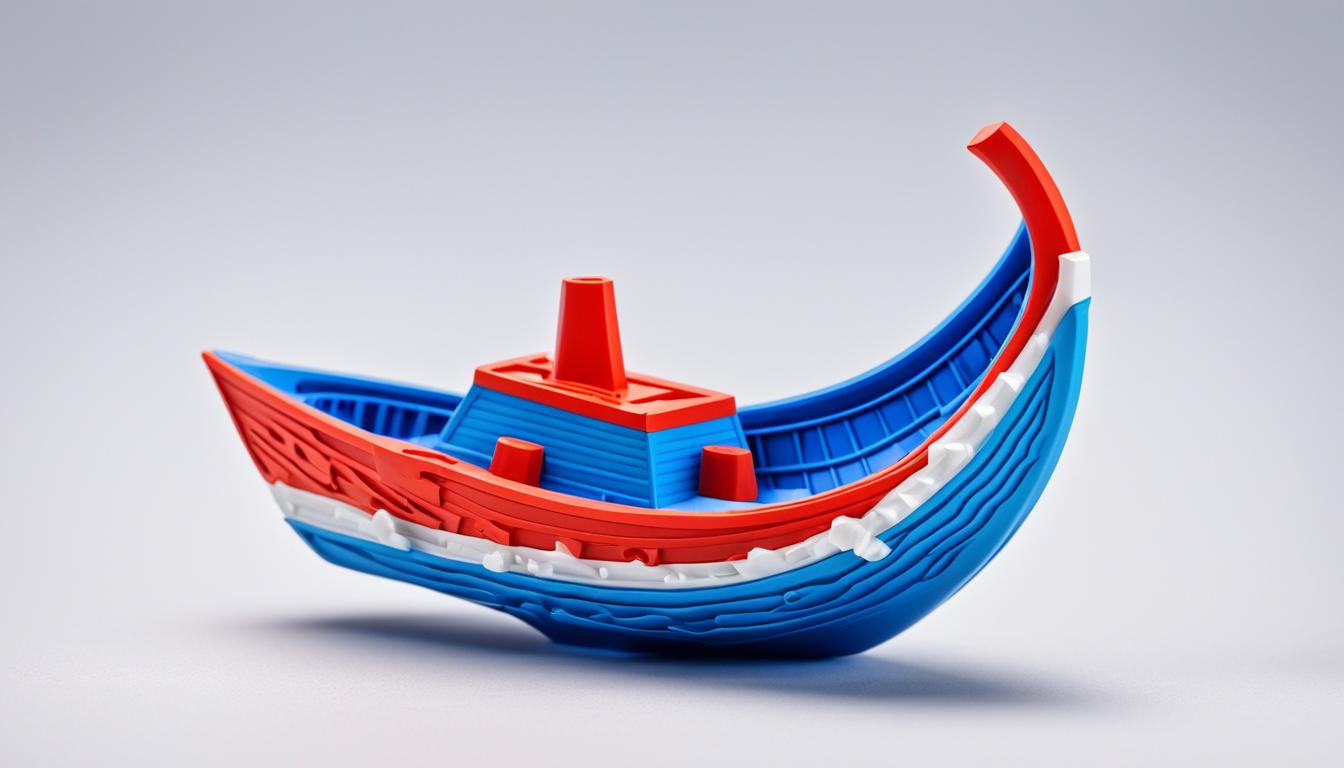
The 3DBenchy, a small tugboat model, serves as a universal benchmark for evaluating and calibrating Fused Deposition Modeling (FDM) 3D printers. This meticulously designed model incorporates numerous challenging geometric features, allowing engineers and hobbyists to diagnose and fine-tune printer performance with a single print. It is widely considered the most 3D printed object globally, a testament to its utility.
Printing the 3DBenchy without supports is crucial for an accurate assessment, as its design inherently tests a printer’s ability to handle complex geometries independently. This comprehensive test helps identify issues ranging from dimensional accuracy to surface finish, providing a holistic view of a printer’s capabilities.
Assessing Overhang Performance on the 3DBenchy
Overhang quality is a critical indicator of a 3D printer’s cooling efficiency and its ability to deposit material accurately on unsupported angles. The 3DBenchy features several challenging overhangs, notably the bow (front hull) and the cabin roof. The bow has a steep 40° overhang angle to the horizontal plane, while the cabin roof slopes at a 5.5° angle.
Inspect the underside of the bow for signs of sagging, curling, or rough textures. These imperfections typically indicate insufficient cooling, where the extruded plastic does not solidify quickly enough before the next layer is deposited. Adjusting the part cooling fan speed, often to 100% for PLA, or reducing the print speed for outer walls can mitigate these issues.
The cabin’s window arches also present overhang challenges, revealing how well the printer manages unsupported sections. Droopy or messy lines in these areas suggest that cooling or print speed parameters require further optimization. Lowering the nozzle temperature slightly can also help, though this should be a last resort to avoid compromising layer adhesion.
Precise Dimensional Tolerance Measurement
| Calibration Parameter | 3DBenchy Feature Tested | Common Issue | Slicer Adjustment |
|---|---|---|---|
| Part Cooling | Bow Overhang, Cabin Arches | Sagging, Curling, Roughness | Increase fan speed, Reduce print speed on outer walls |
| E-steps & Flow Rate | Dimensional Accuracy, Hull Surfaces | Inaccurate dimensions, Over/Under-extrusion | Calibrate E-steps, Adjust extrusion multiplier |
| Retraction Settings | Cabin Windows, Mast | Stringing, Oozing | Adjust retraction distance/speed, Lower nozzle temperature |
| Bridging Settings | Cabin Roof | Drooping, Gaps in bridges | Maximize cooling, Reduce bridge speed, Adjust bridge flow |
| Temperature | Layer Adhesion, Surface Finish | Weak layers, Blobs, Matte/Glossy finish | Adjust hotend temperature (use temp tower) |
Achieving accurate dimensions is paramount for functional 3D printed parts, especially those intended for assemblies or mechanical fits. The 3DBenchy provides numerous features for precise measurement using digital calipers.
Key dimensions to measure include the overall length (60.00 mm from bow to stern), overall width (31.00 mm from port to starboard), and overall height (48.00 mm from bottom to the top of the chimney). The cargo box on the deck measures 12.00 x 10.81 mm externally and 8.00 x 7.00 mm internally, with a depth of 9.00 mm.
FDM 3D printing typically achieves dimensional accuracy of ±0.5% with a lower limit of ±0.5 mm for prototyping, though well-calibrated machines can reach ±0.3 mm for features under 100 mm. Industrial-grade FDM systems, with rigorous calibration, can consistently achieve ±0.05 mm. Consistent deviations from the nominal dimensions indicate a need for E-steps calibration and flow rate adjustments in the slicer.
Evaluating Stringing and Bridging Artifacts
Stringing and bridging are common FDM print defects that the 3DBenchy is specifically designed to highlight. Stringing, characterized by thin plastic strands across gaps, often appears between the cabin windows and around the mast.
This issue typically stems from incorrect retraction settings (distance and speed) or an excessively high hotend temperature. Adjusting retraction distance and speed incrementally, along with optimizing travel speeds and potentially lowering the nozzle temperature, can significantly reduce stringing.
Bridging, the ability to print horizontally over open space without support, is tested by the flat roof of the cabin. Sagging or gaps in this area indicate poor bridging performance. Maximizing part cooling, reducing print speed for bridges, and fine-tuning the bridge flow rate in the slicer are effective solutions.
Analyzing Surface Finish and Layer Adhesion
The aesthetic quality and structural integrity of a 3D print are heavily influenced by its surface finish and layer adhesion. The 3DBenchy’s smooth hull surfaces and detailed features, like the stern nameplate, are excellent for revealing imperfections.
Visible layer lines are inherent to FDM, but excessive roughness, inconsistent finishes, or ‘ghosting’ (faint repetitions of features) point to issues. Over-extrusion can lead to bulging walls and surface blobs, while under-extrusion results in gaps and weak layers. Adjusting the extrusion multiplier and ensuring proper E-steps calibration are crucial for consistent material flow.
Poor layer adhesion, where layers separate, can be caused by low print temperatures or insufficient cooling. Conversely, excessive cooling or too low a temperature can lead to a matte finish, while higher temperatures often yield a glossier surface. The small, extruded letters on the stern, just 0.1 mm thick, also test the printer’s ability to produce fine details and first-layer quality.
Diagnosing Slicer Calibration Issues
The 3DBenchy serves as a comprehensive diagnostic tool for various slicer calibration parameters, integrating all the previously discussed aspects. A systematic approach to calibration is essential to avoid random tweaking.
Initial checks should always include frame stability, belt tension, and bed leveling, followed by Z-offset verification. Subsequent steps involve calibrating E-steps (extruder steps per millimeter) to ensure accurate filament delivery, then fine-tuning the flow rate (extrusion multiplier) to prevent over or under-extrusion.
Temperature towers and retraction towers are valuable calibration prints that complement the 3DBenchy, allowing for precise optimization of hotend temperature and retraction settings for specific filaments. Consistent calibration, especially when changing filaments or hardware, ensures reliable and high-quality prints over time.