
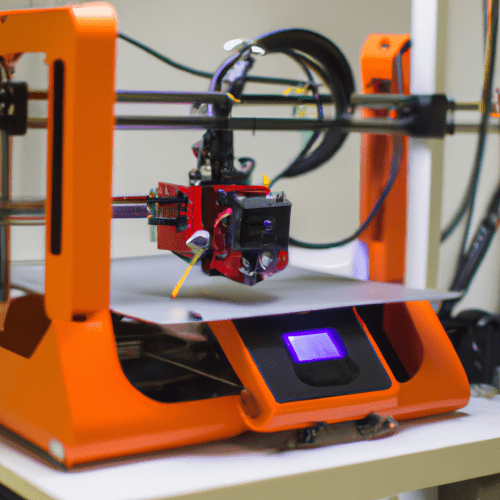
Fused Deposition Modeling (FDM) 3D printing offers an accessible entry point into additive manufacturing, transforming digital designs into physical objects layer by layer. This technology is widely adopted by hobbyists and professionals due to its relative simplicity and cost-effectiveness. Understanding the core components and processes is essential for successful prints and consistent results.
Modern FDM printers have significantly advanced, moving from complex, manual calibration to highly automated systems. Today’s entry-level machines are often plug-and-play, reducing the initial learning curve and allowing users to focus on design and slicing rather than constant hardware adjustments.
Selecting an FDM Printer
Choosing an FDM printer involves evaluating several key features that impact performance, ease of use, and material compatibility. For beginners, printers offering automatic calibration, user-friendly software, and reliable out-of-the-box performance are highly recommended.
Popular choices in 2026 for beginners include the Bambu Lab A1 series (A1 or A1 mini) and the Creality Ender-3 V3 SE. The Bambu Lab A1 mini, for instance, offers full auto-calibration and a quick 15-minute setup, making it an excellent ‘first printer’ option. These machines often feature strain-gauge auto-bed leveling, vibration compensation (input shaping), and dual-gear direct drive extruders, which are fundamental for accurate, high-strength parts.
Consider the build volume required for your projects; smaller printers like the Bambu Lab A1 mini (180 x 180 x 180 mm) are suitable for learning, while larger options like the Bambu Lab A1 (256 x 256 x 256 mm) or Anycubic Kobra X (260 x 260 x 260 mm) provide more versatility. Enclosed printers, such as the Elegoo Centauri Carbon 2 Combo, are beneficial for printing materials like ABS or ASA, which require controlled environments to prevent warping.
Slicer Setup Basics
| Parameter | Typical Range (PLA) | Notes |
|---|---|---|
| Nozzle Diameter | 0.4 mm (standard) | 0.2-0.3mm for fine detail, 0.6-0.8mm for speed/strength. |
| Layer Height | 0.1 mm – 0.3 mm | 0.2 mm offers a good balance of speed and detail. |
| Nozzle Temperature | 190°C – 220°C | Most PLA prints well around 210°C. |
| Bed Temperature | 40°C – 60°C | Not strictly required for PLA, but improves first layer adhesion. |
| Print Speed | 40 mm/s – 150 mm/s | Optimal speeds vary by printer and desired quality. |
| Filament Diameter | 1.75 mm (standard) | Also 2.85mm for some older/industrial printers. |
| Dimensional Tolerance | ±0.2 mm to ±0.5 mm | Desktop FDM; depends on part size, geometry, and orientation. |
| Minimum Wall Thickness | 1.0 mm | Thinner walls may result in fragile parts or gaps. |
| Minimum Detail Size | 0.6 mm | Smaller details may not resolve clearly. |
Slicer software acts as the crucial bridge between your 3D model and the physical print, converting STL or 3MF files into G-code instructions for the printer. The choice of slicer can significantly influence print quality, making it a critical aspect of the 3D printing workflow.
For most FDM users in 2026, OrcaSlicer is a top recommendation due to its built-in calibration tools, broad printer support, and frequent updates. Bambu Studio is optimized for Bambu Lab printers and their multi-color AMS system, while Ultimaker Cura remains a widely used and beginner-friendly option with extensive printer profiles.
Key slicer settings include layer height, infill density, print speed, nozzle temperature, and bed temperature. Layer height, typically ranging from 0.1 mm to 0.3 mm for FDM, directly impacts print detail and time; smaller layers yield smoother, more detailed prints but take longer. Infill density, often set at 20% for general parts, determines the internal structure and strength.
Calibrating the Print Bed
Achieving a perfectly level print bed is paramount for successful FDM printing, ensuring optimal first-layer adhesion and preventing print failures. Modern printers often integrate automatic bed leveling systems, significantly simplifying this process.
Even with auto-leveling, understanding the principles of bed calibration is beneficial. The goal is to ensure a consistent gap between the nozzle and the print surface across the entire build plate. This gap, often referred to as the ‘Z-offset,’ is critical for proper filament squish and adhesion.
Manual calibration typically involves adjusting leveling screws at multiple points on the bed while using a feeler gauge or a piece of paper to set the correct nozzle height. The paper method involves moving the nozzle until it lightly drags on the paper, indicating an appropriate gap. For printers with automatic systems, periodic checks and fine-tuning of the Z-offset may still be necessary to compensate for minor variations.
Sourcing PLA Filament
Polylactic Acid (PLA) is the most popular 3D printing material, favored for its ease of printing, affordability, and biodegradability. It is derived from renewable resources like corn starch or sugarcane and produces minimal odors or toxic fumes during printing, making it suitable for various environments.
The standard filament diameter for FDM printers is 1.75mm, used by approximately 85-89% of home 3D printers. While 2.85mm (often incorrectly labeled as 3mm) is also available, 1.75mm offers improved extrusion control and broader material variety.
When selecting PLA, prioritize brands known for tight diameter tolerance (±0.05mm or better) and consistent quality. Reputable brands in 2026 include Polymaker, Prusament, Hatchbox, eSUN, and Bambu Lab PLA Basic. These brands often provide consistent color, reliable extrusion, and good layer adhesion.
Proper storage of PLA filament is crucial to maintain its printability. PLA is hygroscopic, meaning it absorbs moisture from the air, which can lead to issues like stringing, bubbling, and poor layer adhesion. Store filament in airtight containers with desiccant packs, maintaining a relative humidity below 50%. If filament becomes wet, drying it in a food dehydrator or filament dryer at around 45°C for 4-6 hours can restore its properties.
Downloading 3D STL Models
Accessing 3D models is the initial step in bringing your ideas to life with an FDM printer. The most common file format for 3D printing is the STL (stereolithography) file, which represents the surface geometry of a 3D object using a collection of triangular facets.
Numerous online repositories offer vast libraries of free and paid STL models. Popular platforms include Thingiverse, Printables, MyMiniFactory, and Cults3D. These sites host a diverse range of designs, from functional parts and prototypes to artistic creations and miniatures.
When downloading models, consider the intended scale and complexity. Some models may require minor repairs or adjustments in a mesh editing tool like Meshmixer before slicing to ensure printability. Always check for user comments or reviews regarding print success rates and any recommended print settings for specific models.
The following table outlines typical FDM printing parameters and tolerances: