
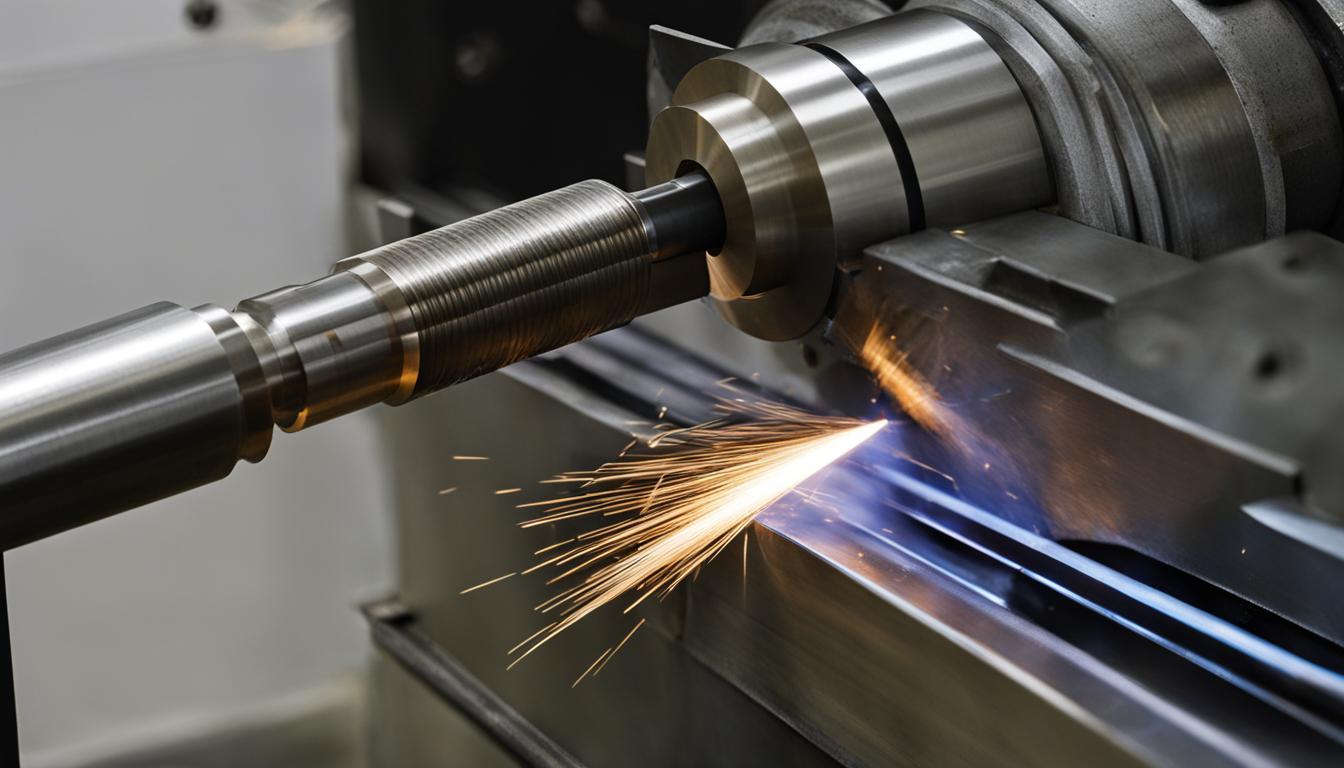
A centre lathe, also known as a manual, universal, or engine lathe, is a foundational machine tool used to produce cylindrical parts by rotating a workpiece against a stationary cutting tool. This versatile equipment is essential in various workshops, from educational settings to industrial repair facilities. It facilitates operations such as turning, facing, drilling, boring, reaming, and thread cutting.
Unlike Computer Numerical Control (CNC) lathes, which rely on automated programming, manual lathes require direct operator control over tool movement and spindle speed. This hands-on approach provides unique benefits, particularly for specific production scenarios and skill development.
High Versatility for Single Parts
Centre lathes excel in producing single, custom, or prototype parts due to their inherent flexibility. Machinists can make real-time adjustments to the cutting process, adapting to unforeseen circumstances or design changes without the need for extensive reprogramming. This adaptability is crucial for ‘one-off’ jobs where setup time for CNC machines would be disproportionately long.
The manual control allows for a high degree of finesse and direct engagement with the material, enabling operators to ‘feel’ the cut and respond instantly to material behavior. This tactile feedback is invaluable for achieving specific surface finishes or navigating complex geometries on unique components.
Manual lathes support a broad range of operations, including parallel turning, taper turning, knurling, parting off, and drilling. This comprehensive capability makes them suitable for diverse tasks, from crafting intricate jewelry to machining shafts for small motors.
Lower Initial Equipment Cost
| Parameter | Mild Steel (HSS Tooling) | Aluminum (Carbide Tooling) | Typical Manual Lathe Tolerance |
|---|---|---|---|
| Cutting Speed (SFM) | 100-200 | 600-1200 | N/A |
| Roughing Feed Rate (IPR) | 0.005-0.015 | 0.004-0.010 | N/A |
| Finishing Feed Rate (IPR) | 0.002-0.005 | 0.002-0.005 | N/A |
| Depth of Cut (Roughing) | 0.020-0.100″ | 0.020-0.150″ | N/A |
| Typical Achievable Tolerance | N/A | N/A | ±0.001″ to ±0.005″ |
Investing in a centre lathe typically involves a significantly lower initial capital outlay compared to its CNC counterparts. Manual lathes generally range from $1,000 to $10,000, with some basic models starting around $5,000. In contrast, CNC lathes can cost between $20,000 and $100,000, or even up to $200,000+ for advanced specifications.
This cost-effectiveness makes manual lathes an attractive option for small workshops, educational institutions, hobbyists, and businesses with limited budgets. The simpler mechanical and electrical systems also contribute to lower maintenance costs and reduced downtime over the machine’s lifespan.
For projects requiring fewer than 100 parts, manual lathes are often more economical on a per-part basis, as they avoid the substantial setup and programming costs associated with CNC production. This makes them ideal for prototyping and small-batch manufacturing.
Simple Manual Operational Control
Operating a centre lathe involves direct manipulation of handwheels and levers, providing immediate control over the carriage, cross-slide, and compound rest movements. This direct interface fosters a deep understanding of machining fundamentals, tool geometry, and material science.
The learning curve for manual lathes is generally moderate, typically requiring 3-6 months to gain proficiency. This contrasts with the steeper 6-12 month learning curve often associated with CNC programming and operation. New machinists develop essential skills like tool sharpening, precise measurement, and understanding cutting forces.
Safety protocols are paramount when operating manual lathes. Operators must always wear appropriate Personal Protective Equipment (PPE), including safety glasses and snug-fitting clothing, and ensure chuck keys are removed before starting the machine. Awareness of hot, sharp chips and proper chip removal techniques are also critical.
Wide Range of Thread Cutting Options
Centre lathes offer extensive capabilities for cutting various internal and external threads, including standard inch (e.g., Unified National) and metric threads. This is achieved by synchronizing the spindle’s rotation with the linear travel of the lead screw through a change-gear train.
When the quick-change gearbox cannot produce a specific thread pitch, machinists can utilize a ‘four-gear’ or ‘compound’ arrangement. This involves calculating and selecting specific gear combinations to achieve the target ratio between the spindle and leadscrew, allowing for highly customized thread forms.
The ability to manually adjust gear ratios and tool paths provides unparalleled flexibility for producing non-standard threads or repairing damaged threads on existing components. This level of control is a significant advantage for specialized applications where off-the-shelf solutions are unavailable.
Ideal for Custom Repair Jobs
Manual lathes are exceptionally well-suited for custom repair and maintenance tasks. Their versatility allows for the precise modification of existing components, such as cylinders, motors, or shafts, to restore functionality.
When a unique or obsolete part breaks, a centre lathe enables machinists to reverse-engineer and fabricate a replacement without the need for complex CAD/CAM programming. This capability is invaluable in industries where rapid, on-demand repairs are critical to minimize downtime.
The hands-on nature of manual machining means that variations between parts are often acceptable or even desired, particularly for repair work where a perfect ‘handmade’ fit is more important than mass-produced uniformity. This makes them indispensable for bespoke solutions.
Technical Parameters and Tolerances
Achieving precision on a manual lathe requires careful attention to speeds, feeds, and depth of cut, which vary significantly based on material and tooling. Operators must select appropriate parameters to ensure optimal material removal, surface finish, and tool life.
Feed rate should generally be less than half the tool’s nose radius to ensure proper chip formation and prevent rubbing. For instance, a tool with a 0.015″ nose radius should have a maximum feed rate of 0.007″ per revolution. Lighter feeds are used for finishing cuts to achieve a finer surface finish.
Spindle speed (RPM) calculations are critical, determined by the desired surface feet per minute (SFM) and the workpiece diameter. For aluminum with HSS tooling at 200 SFM, a 2″ diameter workpiece would require approximately 400 RPM. Modern manual lathes often provide a wide speed range, from 50 RPM for large-diameter roughing to over 2,500 RPM for small-diameter finishing.