
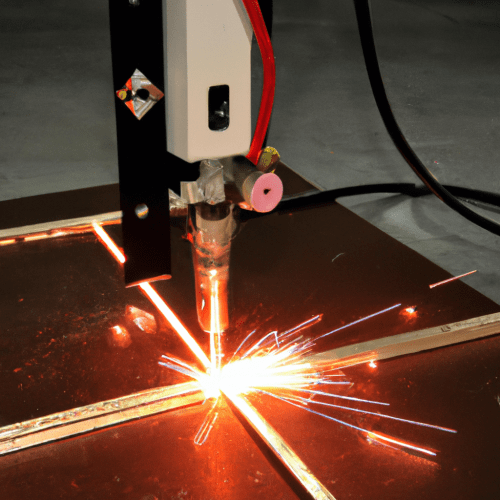
Effective plasma cutting operations demand a precise understanding of the necessary equipment and safety protocols. Achieving clean, accurate cuts on various conductive metals relies heavily on selecting the right components and maintaining them diligently. This guide details the core elements required for a functional and safe plasma cutting setup.
Power Supply Unit
The power supply unit forms the core of any plasma cutting system, converting incoming electrical current into the high-voltage, high-frequency output needed to initiate and sustain the plasma arc. Modern plasma cutters predominantly utilize inverter technology, which offers significant advantages over older transformer-based designs. Inverter systems convert input power to high-frequency AC, then rectify it to DC, employing smaller, lighter components.
Inverter-based units provide superior arc stability and precise current control across the entire amperage range, leading to cleaner starts and reduced consumable wear. This technology also enables multi-voltage input capabilities, allowing units to auto-sense 120V or 230-240V, enhancing job-site flexibility. Energy efficiency is another key benefit, translating into lower operating costs and less heat generation.
A critical specification for any power supply is its ‘duty cycle’, which indicates how long the machine can operate continuously at a given output current within a 10-minute period before requiring a cooldown. For instance, a 60% duty cycle at maximum output means six minutes of cutting followed by four minutes of rest. Professional applications often demand higher duty cycles, typically 60% or more, to maintain productivity.
Output current, measured in amperes, directly correlates with the maximum material thickness a plasma cutter can efficiently process. Higher amperage allows for cutting thicker metals and achieving faster cut speeds. The rated output voltage, proportional to arc length, also influences the system’s ability to cut thicker materials effectively.
Compressed Air Compressor
| Cutting Application | Recommended CFM @ 90 PSI | Minimum Tank Size |
|---|---|---|
| Thin Gauge (up to 1/4 inch) | 5-10 CFM | 20-30 Gallons |
| Medium Gauge (1/4 to 1/2 inch) | 10-12 CFM | 50-80 Gallons |
| Thick Gauge (1/2 inch and above) | 15+ CFM | 80+ Gallons |
A reliable compressed air compressor is indispensable for air plasma cutting systems, as it supplies the gas that forms the plasma arc and blows away molten metal. The compressor’s capacity must match or exceed the plasma cutter’s air demand, typically specified in Cubic Feet per Minute (CFM) at a certain Pounds per Square Inch (PSI).
Most handheld air plasma systems operate optimally around 70-80 PSI, with some requiring up to 120 PSI for thicker materials. For example, a small cutter might need 4 CFM at 80 PSI, while larger units could demand 6.7 CFM at 90 PSI or even 15 CFM or higher for thick gauge cutting. Insufficient CFM or PSI will lead to unstable arcs, poor cut quality, and frequent shutdowns.
Air quality is paramount; plasma cutting requires clean, dry air to prevent premature consumable wear and potential damage to the plasma cutter. Moisture and oil particles in the compressed air can significantly degrade cut quality and shorten consumable lifespan. Therefore, an air dryer or a multi-stage filtration system is essential to remove moisture and oil.
Compressor tank size, while not as critical as CFM and PSI, provides a buffer of compressed air, allowing the compressor motor to cycle less frequently. A minimum 50-liter tank is generally recommended for plasma cutting to ensure pressure stability and reduce wear on the compressor. Rotary screw compressors offer consistent airflow and quieter operation for heavy-duty use, while reciprocating piston compressors are more common and affordable for general use.
Torch Consumables
Plasma torch consumables are the components at the front end of the torch that directly interact with the plasma arc and workpiece, and thus wear out over time. These parts are crucial for generating, focusing, and protecting the plasma arc, directly impacting cut quality and efficiency. Regular inspection and timely replacement are vital for optimal performance.
The five primary consumables include the electrode, nozzle, swirl ring, shield cap, and retaining cap. The electrode, typically made of copper with hafnium or tungsten inserts, carries the negative charge and helps stabilize the arc. The nozzle, often copper or brass, constricts and focuses the plasma arc into a narrow, powerful stream for precise cutting.
A swirl ring, usually made of insulating composites or ceramics, controls and swirls the plasma gas around the arc, enhancing stability and cooling the nozzle. The shield cap protects the nozzle from molten metal spatter and debris, while the retaining cap holds all the consumable parts securely in place within the torch. These components are designed to wear, and their degradation directly affects cut quality, arc starting, and overall torch lifespan.
Grounding Clamp
A robust grounding clamp is fundamental for both operator safety and the proper functioning of a plasma cutter. It completes the electrical circuit, allowing the cutting current to flow from the torch through the workpiece and back to the power supply. An inadequate or improperly connected ground can lead to poor cut quality, arc instability, and significant safety hazards, including electric shock.
The grounding clamp should be securely attached directly to the workpiece or the cutting table, ensuring excellent electrical contact. Avoid attaching the clamp to a part of the material that will be cut off, as this can break the circuit during the cut. For CNC plasma systems, proper grounding involves a ‘star ground’ point, where multiple ground connections converge, often on the cutting table.
Wire gauge for grounding cables is critical and must be appropriate for the maximum current capabilities of the plasma power supply. Using undersized wire can lead to overheating and an ineffective ground path. For instance, a 10 AWG wire is rated for 30 amps, while a 4 AWG wire can handle up to 70 amps. All hardware used in the ground system should ideally be brass or copper to ensure optimal conductivity and corrosion resistance.
Protective Eye Safety Gear
Protecting the eyes from the intense ultraviolet (UV), infrared (IR), and visible light radiation emitted during plasma cutting is non-negotiable. The bright plasma arc can cause severe eye damage, including ‘arc eye’ (photokeratitis), long-term strain, and cataracts, without proper protection. Therefore, appropriate eye safety gear, primarily a welding helmet, is essential.
Auto-darkening welding helmets are highly recommended for plasma cutting. These helmets feature lenses that automatically darken to a pre-selected shade level within milliseconds of detecting an arc, then return to a lighter state when the arc ceases. This technology allows operators to maintain visibility before and after the cut without repeatedly lifting and lowering the helmet, improving efficiency and safety.
The required shade level for plasma cutting varies depending on the amperage. For low to moderate current plasma arc cutting, shades 8-9 are typically used. Higher current applications, especially above 300 amps, necessitate darker shades, ranging from 10 to 14. Always consult the plasma cutter’s manual and relevant safety standards, such as ANSI Z87.1, for specific recommendations.
Beyond the helmet, additional personal protective equipment (PPE) is crucial. This includes safety glasses worn under the helmet for continuous protection, flame-resistant clothing, welding gloves, and steel-toed shoes. Ensuring all protective gear meets current safety standards provides comprehensive protection against sparks, molten metal, and radiation, safeguarding the operator during all cutting operations.